Connect Factory Systems Into One Dashboard: A Data-Ownership Map
Connect Factory Systems Into One Dashboard. Use a worked manufacturing test, exception checks and direct Optiwise workflow evidence before rollout.
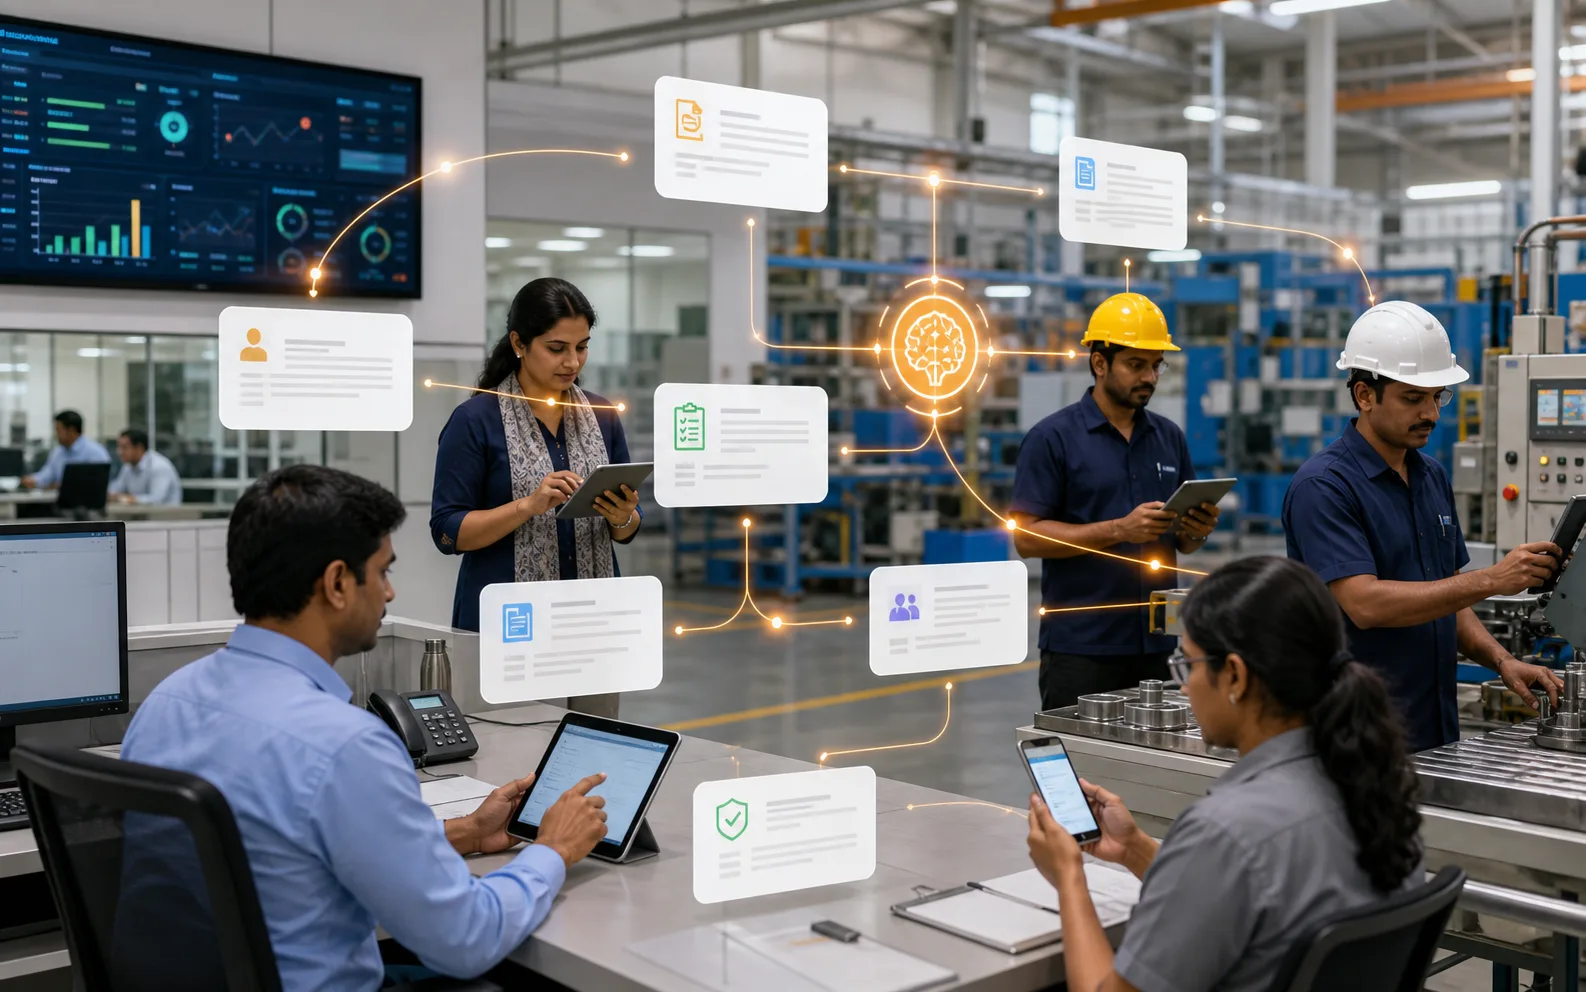
Connect Factory Systems Into One Dashboard: A Data-Ownership Map helps you join ERP, shop-floor, quality and machine data without duplicating truth. Start with one order, one item and one exception. A screen tour cannot prove that records stay connected when the work changes.
The ERP owns the work order, the machine gateway records runtime, and quality owns disposition. The dashboard may display all three, but a correction must return to the owning record rather than editing a copied total.
Start with the decision the system must support
Assign one system of record to every field and define how timestamps, IDs and corrections travel.
Optiwise combines operational records with OptiEdge machine capture, device-to-machine mapping, configurable no-code modules, automations and webhooks. Field-level integration still requires an acceptance design.
Use ISA-95 enterprise and control-system model as an external reference for the relevant data or process model. It does not prove an Optiwise feature or a business result; the product statements above come from our current feature record.
| # | Input to prepare | Evidence to retain |
|---|---|---|
| 1 | System of record by field | Owner and last update |
| 2 | Shared item, machine and order IDs | Definition and source |
| 3 | Update direction and frequency | Acceptance rule |
| 4 | Failure, retry and reconciliation owner | Exception owner |
Run one controlled workflow before expanding scope
- 1. System of record by field. Confirm who maintains it and which record is authoritative.
- 2. Shared item, machine and order IDs. Use the current value in the chosen test order.
- 3. Update direction and frequency. Record the pass condition before the demo begins.
- 4. Failure, retry and reconciliation owner. Assign the person who resolves a mismatch.
Keep the first test small enough to reconcile by hand. When the system result differs from the source documents, stop and identify whether the problem is master data, timing, transaction ownership or configuration.
Test exceptions alongside the normal flow
- Duplicate event arrives
- Device maps to wrong machine
- One system commits before another fails
For each exception, record the expected status, permitted action, approver and audit trail. A useful manufacturing system should make the exception visible without allowing an unapproved shortcut to rewrite history.
Verify the connected Optiwise workflow
Review workflow details, product capability, supporting guide, implementation context, connected process, book a demo. In the demo, ask us to execute the scenario with your roles and sample records. Confirm the source transaction, resulting status, notification or action, correction method and report before accepting the workflow.
Questions to ask before rollout
What should we test first?
Choose one current order with a known complication. Prepare the four inputs above, run the transaction sequence and reconcile the result with the source documents.
What result should we accept?
Accept the workflow only when the normal path and named exceptions leave a complete, role-appropriate record. Keep feature validation separate from a promised business outcome.
You connect all factory systems into one dashboard by first defining the decisions the dashboard must support, then connecting the core operational data: production status, inventory, material issue, quality, maintenance, dispatch, and cost signals. The goal is not to put every number on one screen. The goal is to create one reliable operating picture of the factory.
Many manufacturers run their factories across separate systems. Production has Excel. Stores has inventory records. Quality has inspection sheets. Maintenance has registers. Dispatch has shipment trackers. Finance has accounting software. Each department may be doing its work, but management still struggles to answer simple questions quickly.
Which orders are delayed? Which material is blocking production? Which machine is down? Which batch is on quality hold? Which finished goods are ready for dispatch? Which jobs are costing more than expected?
A unified dashboard should answer these questions without forcing people to manually reconcile five different sources.
Start With the Business Questions
Do not begin by asking, “What all can we connect?” Start by asking, “What do we need to know every day?”
For most manufacturers, the key questions are:
- What is running right now?
- Which orders are delayed?
- Which machines or lines are stopped?
- Which material shortages affect production?
- Which batches are on quality hold?
- Which orders are ready for dispatch?
- Which jobs are at cost risk?
- Which department owns the next action?
These questions define what the dashboard should pull together.
Identify the Core Data Sources
A factory dashboard usually needs data from several areas.
Production data:
- Work orders
- Line status
- Planned vs actual output
- WIP by stage
- Shift reports
Inventory data:
- Material availability
- Material issue
- Shortages
- Reserved stock
- Packing material status
Quality data:
- Inspection status
- Rejection
- Rework
- Quality holds
- Defect reasons
Maintenance data:
- Machine downtime
- Breakdown reasons
- Preventive maintenance
- Spare readiness
Dispatch data:
- Finished goods
- Packing status
- Due orders
- Ready-to-ship quantity
- Delayed dispatch
Finance or costing signals:
- Material consumption
- Labor or machine time
- Scrap and rework cost
- Job cost variance
The dashboard becomes useful when these data sources are connected around common references such as work order, item, customer order, machine, batch, or material lot.
Use Common IDs Across Systems
System integration fails when departments use different references for the same job. Production may use a work order number, sales may use a customer order number, quality may use a batch number, and dispatch may use an invoice reference.
A good connected dashboard needs common IDs:
- Sales order number
- Work order number
- Item or product code
- Batch or lot number
- Machine or line ID
- Material lot
- Customer reference
Without common references, the dashboard may show data, but it will not tell one connected story.
Clean the Data Before Connecting Everything
A dashboard is only as reliable as the data behind it. If item codes are duplicated, machine names are inconsistent, or status definitions are unclear, integration becomes messy.
Before connecting systems, clean:
- Item masters
- Machine names
- Customer and supplier names
- Work order formats
- Status definitions
- Downtime reasons
- Defect categories
- Material issue rules
This work may feel boring, but it is what makes the dashboard trustworthy.
Choose Between Integration and Consolidation
There are two broad ways to build one dashboard.
Integration means connecting multiple existing systems so their data appears in one reporting layer.
Consolidation means moving key workflows into one ERP or operating system so data is generated in one place from the start.
Integration may be useful when existing tools must remain. Consolidation is often cleaner when spreadsheets and disconnected systems are creating too much manual work.
For growing manufacturers, a connected ERP can reduce the need to maintain many separate tools.
Role-Based Dashboards Matter
One dashboard does not mean one screen for everyone. Different people need different views.
Owner view:
- Production target achievement
- Orders at risk
- Major delays
- Dispatch status
- Cost signals
Production manager view:
- Work order progress
- Line status
- WIP
- Downtime
- Shift output
Stores view:
- Material shortages
- Issue pending
- Reserved stock
- Purchase dependencies
Quality view:
- Inspection pending
- Holds
- Rejection and rework
- Defect trends
Dispatch view:
- Ready goods
- Packing status
- Due orders
- Pending shipments
Role-based dashboards keep the system useful instead of overwhelming.
Build Alerts for Exceptions
A unified dashboard should highlight what needs attention.
Useful alerts include:
- Work order delayed
- Material shortage blocking production
- Machine downtime beyond threshold
- Quality hold on urgent order
- WIP stuck too long
- Dispatch risk
- Preventive maintenance overdue
- Cost variance crossing limit
Alerts should be routed by responsibility. If everyone receives every alert, no one owns the action.
Where AICAN Optiwise Fits
AICAN Optiwise helps manufacturers connect key factory operations into one ERP view: production, inventory, purchase, quality, maintenance signals, dispatch, and reporting. This gives teams one shared operating picture instead of scattered spreadsheets.
With Optiwise, manufacturers can track work orders, material readiness, WIP, downtime, quality holds, dispatch status, and cost-related signals in a structured way. This makes dashboard consolidation more practical because the data comes from connected workflows.
AICAN builds ERP for manufacturers who want clearer factory control without unnecessary complexity. You can learn more on the About AICAN page.
FAQ
Can all factory systems be connected into one dashboard?
Yes, many factory systems can be connected, but the quality of the dashboard depends on clean data, common references, and clear workflows across departments.
What systems should a factory dashboard connect?
A useful dashboard should connect production, inventory, quality, maintenance, dispatch, purchase, and cost or finance signals where relevant.
Is integration better than one ERP system?
It depends. Integration can work when existing systems must stay. A unified ERP is often cleaner when the business relies heavily on spreadsheets and manual reconciliation.
What is the biggest challenge in factory dashboard integration?
The biggest challenge is inconsistent data: different item codes, unclear statuses, duplicate records, and departments using different references for the same job.
Should every user see the same dashboard?
No. Owners, production managers, stores, quality, maintenance, and dispatch teams should have role-based views.
How does ERP help dashboard consolidation?
ERP connects daily workflows so production, inventory, quality, and dispatch data are generated in one system, making dashboards more reliable.
Founder’s Note
A dashboard should not be a collage of disconnected numbers. It should tell the truth of the factory in a way people can act on.
At AICAN, we believe the value of integration is not technical neatness. It is operational clarity. When production, stores, quality, dispatch, and management look at the same facts, the factory becomes easier to run.
Final Thought
Connecting factory systems into one dashboard starts with common questions, common references, and clean workflows. Do not connect everything just because it is possible. Connect what helps the factory make better decisions.
A unified dashboard is valuable when it reduces manual chasing, exposes delays early, and gives every department a shared view of what needs action.
Related Posts
Kanban System | Optiwise
Learn how a Kanban system works in manufacturing, where it helps, where it fails, and how Optiwise connects Kanban signals with inventory, purchase, and production planning.
12 Jun 2026Read more →Erp In Operations Management | Optiwise
Learn how ERP improves operations management by connecting planning, inventory, purchase, production, quality, dispatch, finance, and reporting.
12 Jun 2026Read more →ERP for FMCG Companies in India
A practical guide to ERP for FMCG companies in India, covering distributor orders, batch tracking, expiry, inventory, production, schemes, costing, and reporting.
11 Jun 2026Read more →Optiwise, Odoo, Acumatica and Business Central for Manufacturing
Compare manufacturing workflows in Optiwise, Odoo, Acumatica and Dynamics 365 Business Central. See what your factory can run in Optiwise.
11 Jun 2026Read more →