Optimize Manufacturing Operations: Improve One Constraint With Evidence
Optimize Manufacturing Operations: Improve One Constraint With Evidence. Use a worked factory scenario, explicit inputs and exception checks before rollout.
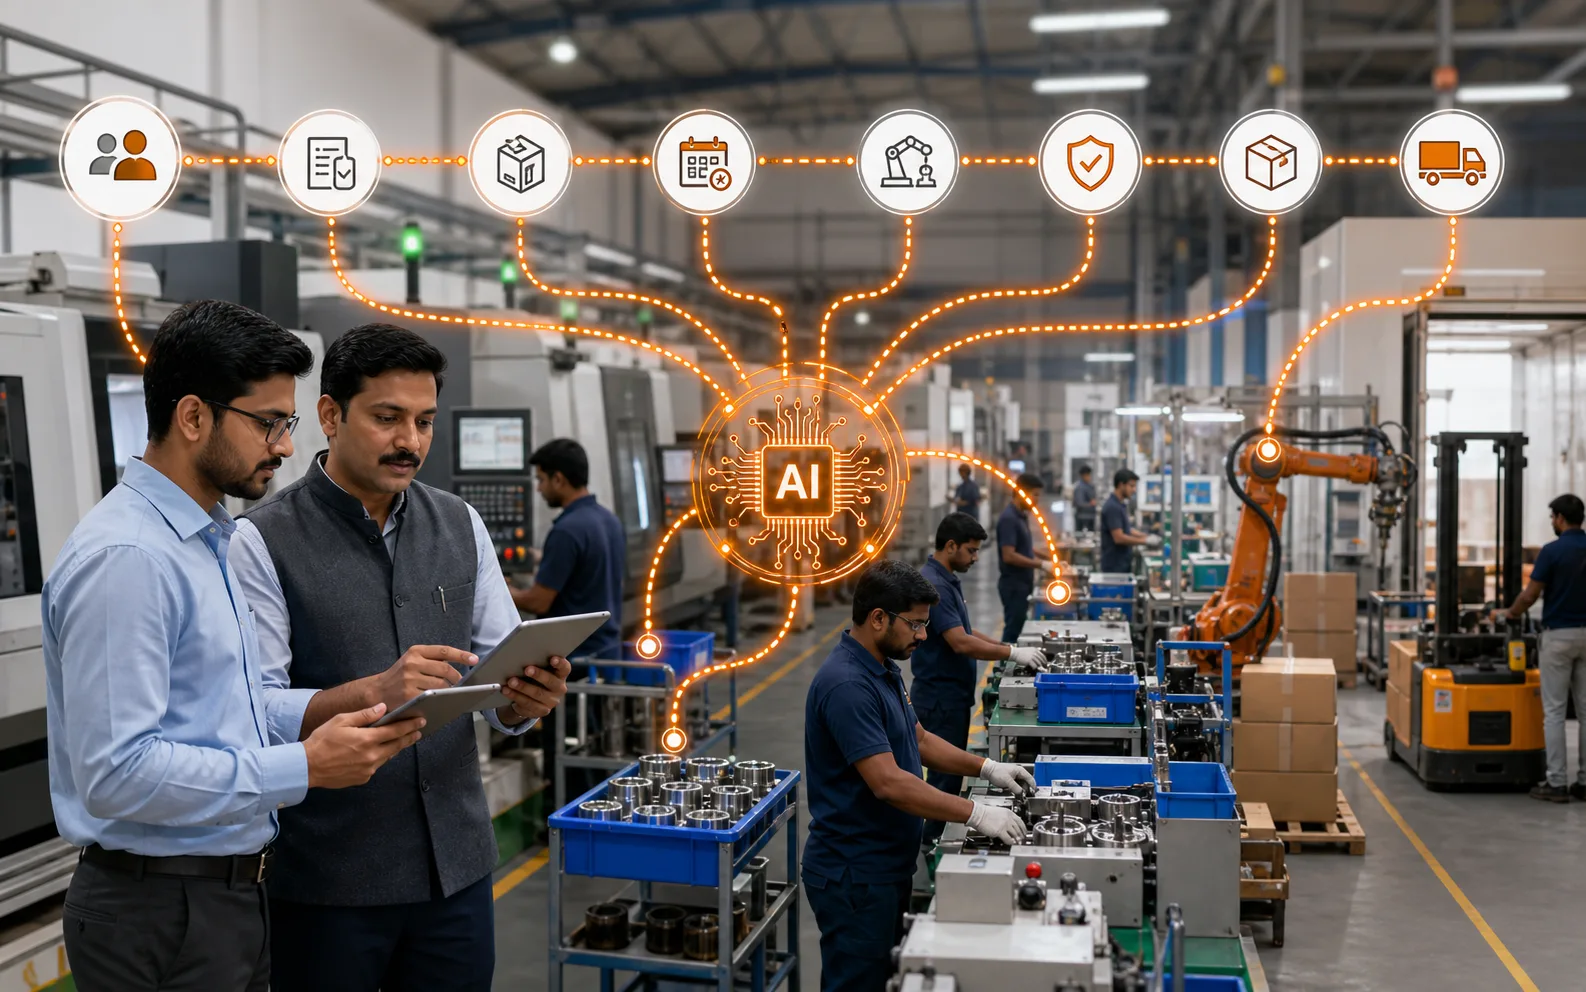
Optimize Manufacturing Operations: Improve One Constraint With Evidence helps you run a bounded improvement cycle on a factory constraint. Use a representative order, the people who perform the work and at least one difficult exception.
A weekly review shows late orders, but the team separates material, capacity, outside-work and quality blockers before choosing an intervention.
Define the decision and its evidence
Define the event and baseline, change one controllable condition, and recheck the same measure.
We connect nested BOMs, routing, machine and worker entries, material consumption, rework, inspection and finished-goods receipt to the manufacturing order.
NIST smart manufacturing program is the external process or vendor reference used for this guide. Vendor documentation records the vendor's stated workflow; our product statements come from our current product record.
| Step | Required input | Evidence to capture |
|---|---|---|
| 1 | Constraint and accountable owner | Named owner and definition |
| 2 | Baseline period and source | Current source record |
| 3 | Intervention and expected signal | Acceptance rule |
| 4 | Review date and stopping rule | Correction and escalation |
Run the workflow with accountable roles
- 1. Constraint and accountable owner. Name the role that owns this record and decision.
- 2. Baseline period and source. Use a current value from the representative order.
- 3. Intervention and expected signal. Write the passing condition before the test.
- 4. Review date and stopping rule. Assign correction and escalation responsibility.
Reconcile the result by hand. When the system differs from the source record, classify the gap as master data, timing, transaction ownership, permissions or configuration before changing the process.
Test the exceptions that disrupt a normal day
- Data definition changes: record the expected status, permitted action, approver, correction path and audit evidence.
- Another intervention overlaps: record the expected status, permitted action, approver, correction path and audit evidence.
- The constraint moves downstream: record the expected status, permitted action, approver, correction path and audit evidence.
A quick normal transaction shows the main path. A controlled exception shows whether the configured workflow can survive real factory conditions.
Connect this task to the operating workflow
review the product workflow, check the connected module, prepare the supporting records, see the control step, read the related guide. Book a connected Optiwise demo and ask us to run your scenario with the normal path, exception and correction.
Questions to settle during the demo
What should we prepare?
Prepare one representative order, the four inputs above and one complication your team encounters today. Remove confidential values while keeping the record relationships intact.
What is a passing result?
Accept the workflow when the normal path and exceptions leave a complete, role-appropriate record another person can reconcile. Validate the configured capability separately from any proposed commercial or operational outcome.
Optimizing manufacturing operations means making the factory run with less waste, fewer delays, better visibility, stronger quality, and more reliable delivery. It is not just about producing faster. A factory can run fast and still lose money if inventory is uncontrolled, quality is unstable, procurement is delayed, or planning is unrealistic.
True optimization connects people, machines, materials, money, and information.
Many manufacturers try to improve one department at a time. Production pushes output. Purchase tries to reduce cost. Stores tries to maintain stock. Sales pushes delivery. Finance watches working capital. But when these teams operate separately, the factory can become busy without becoming efficient.
Optimization starts when the whole system becomes visible.
Start With End-to-End Visibility
You cannot optimize what you cannot see. A factory needs visibility into production status, machine availability, material readiness, purchase delays, quality issues, dispatch plans, and financial impact.
If each department uses separate spreadsheets, messages, and manual updates, management receives a delayed picture. Decisions become reactive.
Connected visibility helps teams understand what is happening now and what may become a problem soon.
Improve Production Planning
Production planning strongly affects operating performance. A plan should consider customer priority, material availability, machine capacity, manpower, quality requirements, tooling, and delivery commitments.
A plan that ignores constraints will fail on the shopfloor.
Good planning also needs feedback. If actual output differs from planned output, the reason should be captured. Was the issue material, machine, manpower, quality, setup, or planning assumption? Over time, this makes planning more realistic.
Balance Inventory Carefully
Inventory optimization is a balance. Too much stock blocks working capital and increases risk of damage or obsolescence. Too little stock stops production and delays customers.
Manufacturers should track fast-moving items, slow-moving items, reorder points, safety stock, vendor lead times, minimum order quantities, and material consumption trends.
AI and ERP systems can help identify risks early, but teams still need discipline in item masters, stock transactions, and purchase planning.
Reduce Downtime and Speed Loss
Operations optimization requires improving machine availability and performance. Downtime, minor stoppages, setup delays, tool change delays, and speed loss all reduce output.
Track downtime by specific reason and machine. Review repeated issues weekly. Connect maintenance with spare planning and production priorities.
A machine running below expected speed can be as damaging as a machine that stops completely.
Strengthen Quality Control
Poor quality creates scrap, rework, customer complaints, delayed dispatch, and hidden cost. Optimization must include first-pass quality improvement.
Track defect reasons, rework, rejection by product, supplier-related issues, machine-wise defects, and corrective actions. Quality data should be specific enough to support root cause analysis.
The goal is not only inspection. The goal is prevention.
Make Procurement More Predictable
Procurement delays can damage production even when the production team is ready. Purchase planning should be connected to inventory, production schedules, vendor lead times, approval workflows, and finance constraints.
A good procurement system helps teams see pending approvals, delayed suppliers, price changes, and material risks before they affect the shopfloor.
Improve Dispatch and Customer Communication
Operations are not optimized if goods are produced but dispatch is delayed due to documentation, packing, approval, or unclear priority.
Sales, production, stores, dispatch, and finance need shared visibility into order status. Customer communication improves when internal status is reliable.
Use Exception-Based Reporting
Managers do not need more reports. They need better exception visibility.
Useful reports show what needs attention: delayed jobs, stock risks, quality issues, overdue purchase orders, pending approvals, dispatch delays, cost variance, and machine downtime.
A good reporting system helps leaders act faster instead of spending time searching for problems.
Build Continuous Improvement Rhythm
Optimization is not a one-time project. It needs a rhythm: daily reviews, weekly root cause meetings, monthly KPI analysis, and regular process improvements.
KPIs should include OEE, on-time delivery, inventory turns, downtime, scrap, rework, purchase delays, production plan adherence, and customer complaints.
How Optiwise Supports the Workflow
AICAN Optiwise helps manufacturers optimize operations through connected workflows across production, inventory, purchase, sales, finance, and reporting.
Instead of isolated department-level data, teams get a shared operational view. AICAN supports manufacturers who want practical control over the full manufacturing flow, from material planning to production, dispatch, and business reporting. Learn more at About AICAN.
Founder’s Note
Optimization is not one big decision. It is hundreds of small decisions made with better visibility.
A connected factory gives people the information they need before problems become expensive. That is where real improvement begins: not in working harder, but in working with clearer signals.
FAQ
What is manufacturing operations optimization?
It is the process of improving production, inventory, procurement, quality, maintenance, dispatch, and reporting so the factory runs more reliably and profitably.
Where should a factory start?
Start with visibility into production status, inventory availability, downtime, purchase delays, and quality issues.
How does ERP help optimize operations?
ERP connects departments and provides real-time operational data, reducing manual follow-ups and improving decision-making.
What KPIs should be tracked?
Track OEE, downtime, plan adherence, on-time delivery, inventory turns, scrap, rework, procurement delays, and working capital impact.
What is the biggest optimization mistake?
Optimizing one department without considering the full workflow. Local improvement can create problems elsewhere if the system is not connected.
Final Thought
Manufacturing optimization is about connected control. Improve visibility, reduce repeated losses, align departments, and use data to make decisions earlier. A factory becomes stronger when every team works from the same operational truth.
Related Posts
A Manufacturing Alternative to SAP: Optiwise
Run your factory in Optiwise, a manufacturing alternative to SAP Business One with connected operations, AI agents and no-code workflows.
14 Jun 2026Read more →How Do I Know If My Manufacturing Business Really Needs an ERP?
A practical guide for manufacturers to identify when spreadsheets, manual follow-ups, and disconnected systems are no longer enough — and when ERP becomes an operational necessity.
14 Jun 2026Read more →Production Management System Optimized | Optiwise
Learn best practices for optimizing a production management system across planning, scheduling, material readiness, quality, and reporting.
12 Jun 2026Read more →
What Is the Best ERP for Pharmaceutical Manufacturing?
Learn how to choose the best ERP for pharmaceutical manufacturing, with guidance on batch control, quality workflows, traceability, inventory, documentation, and GMP discipline.
10 Jun 2026Read more →