How to Reduce Factory Downtime: Diagnose Repeated Losses
Use a reviewed stop log, a worked lost-time comparison and an action register to investigate factory downtime and check whether a change improves the result.
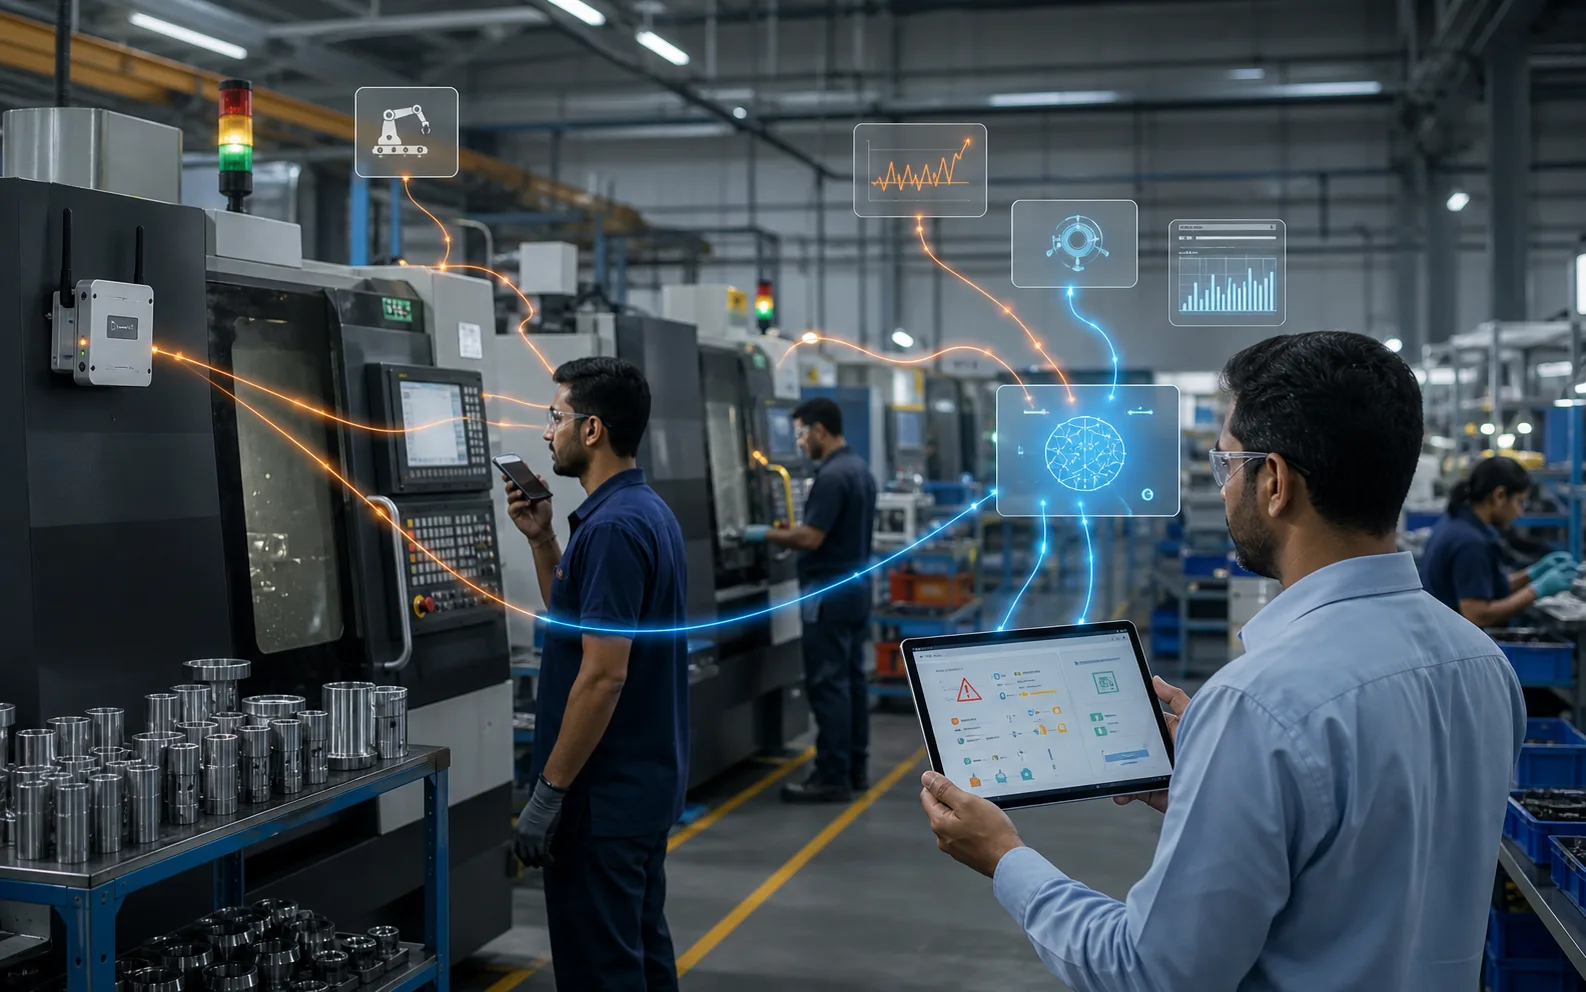
Reduce factory downtime by reviewing reliable stop records, investigating the losses that constrain production and checking corrective actions under comparable operating conditions. A reason code gives you a place to start investigating; it does not prove the root cause.
Begin with one machine or production flow where stops affect the work you need to complete. Include planning, stores, production, quality and maintenance when their records are relevant to the stopped job.
Check the stop log before prioritizing
Confirm the operating window, time boundaries and treatment of setup and planned breaks. Remove duplicate intervals and investigate missing reasons. The CNC downtime log explains how to capture these records without double-counting a stop.
Review the affected job and operation. A long stop on a resource with spare capacity may have a different delivery effect from a shorter stop on the operation that limits output. Keep that context beside the minutes.
Separate frequency from total time
In this illustrative review, the selected operating window includes setup time as a non-running category. The reviewed records contain 120 minutes of setup, 90 minutes of material waiting and 30 minutes of breakdown. Planned breaks are excluded consistently from this example.
| Category | Minutes | Share of the 240-minute total |
|---|---|---|
| Setup | 120 | 50% |
| Material wait | 90 | 37.5% |
| Breakdown | 30 | 12.5% |
| Total | 240 | 100% |
Setup plus material wait accounts for 210 of 240 minutes, or 87.5%. That helps choose an investigation, but it does not establish that all setup time is avoidable or that the breakdown can be ignored. Check bottleneck impact, recurrence and the operating consequences before assigning priority.
Count events as well as minutes. Many brief material waits may need a different response from one late delivery, even when their totals match.
Choose a specific corrective experiment
| Observed issue | Investigation / proposed change | Owner and evidence to review |
|---|---|---|
| Repeated material waits | Trace item, location, reservation and release checks for affected jobs | Stores and planning; compare readiness records and subsequent starts |
| Long setups on repeat parts | Compare planned and actual setup tasks, fixture readiness and instruction changes | Production owner; retain setup observations and approved task changes |
| Repeated alarm stops | Review the fault history and maintenance findings through the approved maintenance process | Maintenance owner; corrective-work record and repeat-event history |
| Quality holds with unclear disposition | Check whether the required inspection input and decision owner were available | Quality owner; hold start, decision and release records |
Write the expected mechanism before making the change. For a material-readiness review, the hypothesis might be that checking the required blank before release will reduce stops caused by missing blanks. Record the scope and the first review date. Avoid changing several unrelated processes and then attributing the result to one of them.
Recheck under comparable conditions
Compare the same machine or workflow, definitions and a similar product mix. Record changes in scheduled time, batch size, number of setups and demand. Fewer stop minutes during a lightly loaded shift do not establish more available production capacity.
Check for displacement: a change that shortens material waiting may move the delay into inspection or create more work in progress. Review the next operation and good output, not only one stop category. Retain unsuccessful trials and decide whether to revise the action or close the hypothesis.
ERPNext’s downtime-entry documentation illustrates a basic machine/minutes record. If you evaluate an Optiwise IoT dashboard, ask how the recorded intervals, reasons and job context can be inspected and exported for this review.
Questions from manufacturing teams
What is the first step in reducing factory downtime?
Establish a consistent stop log with machine, job, duration and observed reason. Review missing or overlapping records before choosing an investigation.
Should I always fix the category with the most minutes first?
Use total minutes alongside recurrence, bottleneck impact and operating consequences. A large category can include necessary work, and a smaller loss can constrain the whole flow.
How do I know a downtime action worked?
Compare the agreed measure before and after under similar conditions, inspect the mechanism and check for delays moved elsewhere. Record uncertainty and unsuccessful trials.
Related Posts
Kanban System | Optiwise
Learn how a Kanban system works in manufacturing, where it helps, where it fails, and how Optiwise connects Kanban signals with inventory, purchase, and production planning.
12 Jun 2026Read more →Erp In Operations Management | Optiwise
Learn how ERP improves operations management by connecting planning, inventory, purchase, production, quality, dispatch, finance, and reporting.
12 Jun 2026Read more →ERP for FMCG Companies in India
A practical guide to ERP for FMCG companies in India, covering distributor orders, batch tracking, expiry, inventory, production, schemes, costing, and reporting.
11 Jun 2026Read more →
Optiwise, Odoo, Acumatica and Business Central for Manufacturing
Compare manufacturing workflows in Optiwise, Odoo, Acumatica and Dynamics 365 Business Central. See what your factory can run in Optiwise.
11 Jun 2026Read more →