CNC Downtime Tracking: Reason Codes and a Shift Log
Record CNC stops with clear reason codes, start/end times, job context and a reconciled shift log. Separate missing signals, idle time and breakdowns.
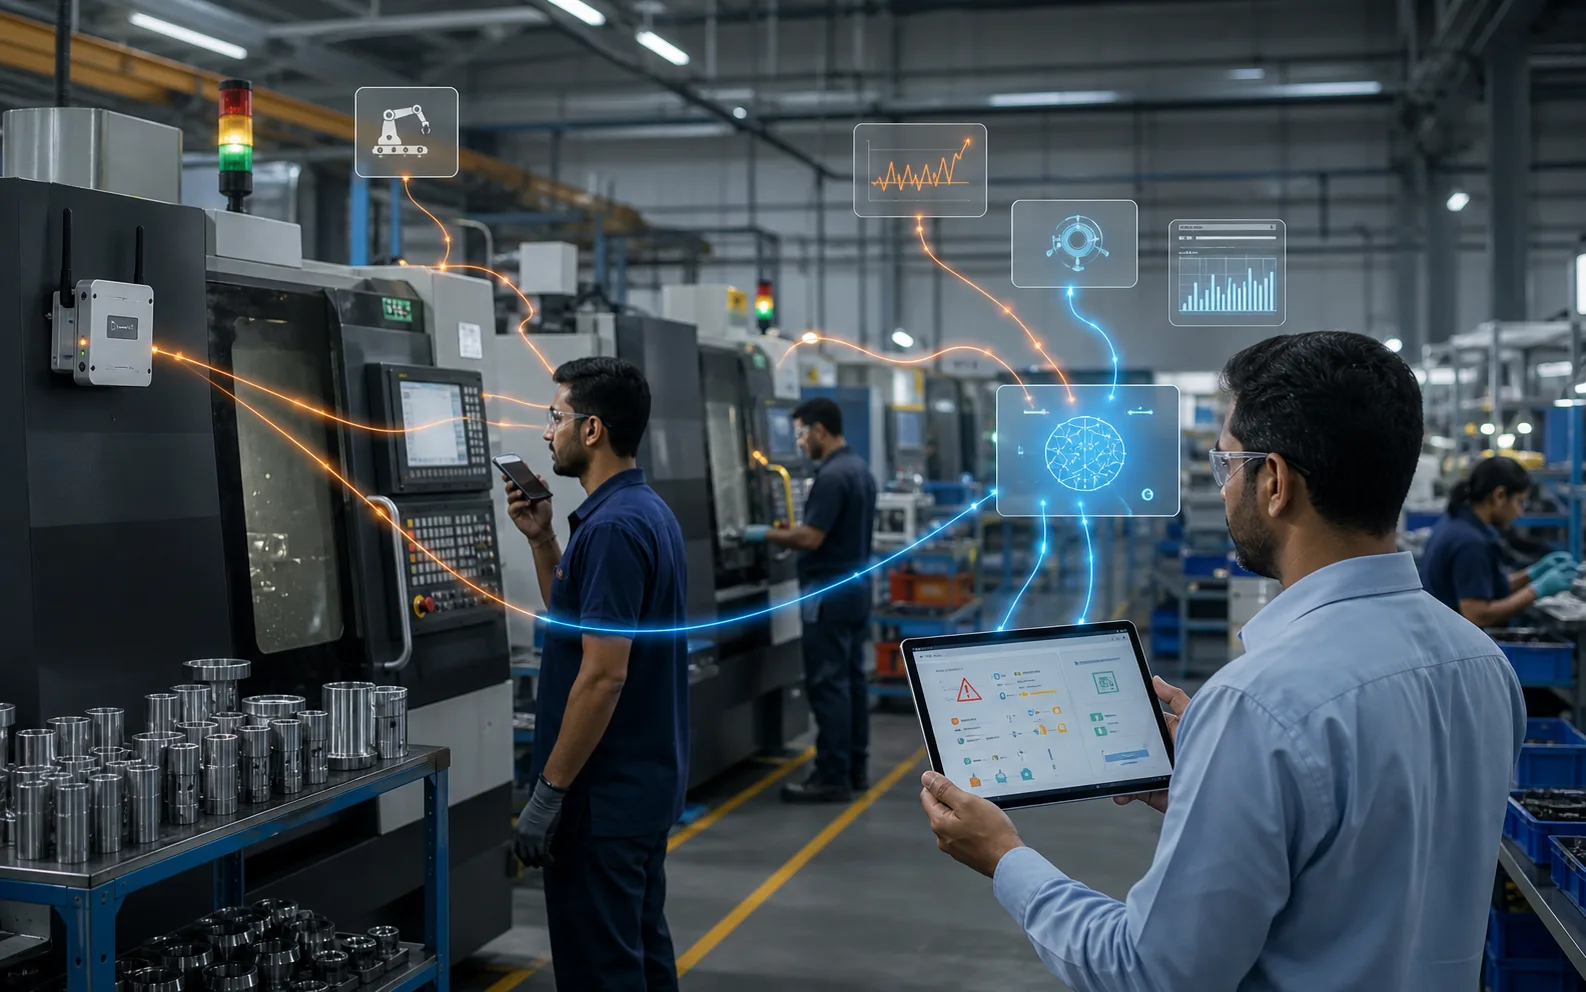
A useful CNC downtime log records the machine, affected job, start and end time, elapsed minutes, reason and review owner for each stop. “Machine stopped” is an observation; it does not establish why production stopped.
Agree the reporting boundary first. State the scheduled operating window, treatment of planned breaks and changeovers, and whether short stops are recorded individually. Keep those definitions consistent when comparing shifts.
Use a small, clear reason-code set
| Category | Evidence to record |
|---|---|
| Machine alarm / breakdown | Observed alarm or symptom and maintenance reference |
| Tool / fixture | Tool or fixture issue; affected job and required follow-up |
| Setup / program | Changeover or program preparation; planned versus additional time |
| Material wait | Missing, wrong or held material and the responsible follow-up |
| Inspection / quality hold | Required check or disposition, with quality owner |
| No released job / resource unavailable | Planning or staffing context rather than assuming a machine fault |
| Unknown / data gap | What is missing and who will investigate |
Make the reason specific enough to act on without asking operators to guess a root cause. An alarm description can support investigation; it is not automatically the final mechanical diagnosis. Preserve the original observation when a reviewer later updates the classification.
Record and reconcile one stop
In this illustrative example, CNC-02 stops at 10:05 and resumes at 10:17 during job WO-104. The elapsed time is 12 minutes. The initial reason is “material wait”; the review records that the correct blank was unavailable at the workstation.
| Field | Illustrative entry |
|---|---|
| Machine / job | CNC-02 / WO-104 |
| Date and timezone | Record the operating date and local timezone |
| Start / end | 10:05 / 10:17 |
| Elapsed minutes | 12 |
| Class / reason | Unplanned stop / material wait |
| Observation / evidence | Required blank unavailable; stores follow-up reference |
| Recorder / reviewer | Named operator and supervisor |
| Disposition | Material supplied; restart recorded; cause investigation assigned |
For a stop crossing midnight, record full dates and times. Split reporting at the shift boundary if needed, while retaining the original event identity so the same minutes are not counted in both shifts.
Handle overlapping reasons explicitly
If a machine waits for material and a tool issue is discovered during the same 12-minute interval, do not add two 12-minute stops for that machine. Keep one time interval with a primary classification and supporting notes, or split it into non-overlapping intervals when the evidence supports that split.
Reconcile stop minutes against the defined shift window. Review gaps, impossible negative durations, repeated event IDs and an end time that precedes the start. Keep planned non-production time separate according to the agreed definition.
Check machine signals before trusting automatic totals
A missing network update should remain a data gap until it is resolved. It does not prove a breakdown. Confirm which signal means running, stopped or disconnected, and compare a sample of recorded intervals with operator observations. Check clock alignment and the process for adding a reason.
ERPNext’s downtime-entry documentation describes a straightforward manual record of machine downtime in minutes. A reliable manual log can establish the definitions before any machine connection is introduced.
Use the downtime improvement guide to choose investigations from the reviewed log. For availability, performance and quality together, see the worked OEE calculation. In an Optiwise IoT discussion, ask which signals and manual inputs your proposed configuration needs.
Questions from manufacturing teams
What should a CNC downtime log contain?
Record machine, job, full start/end times, elapsed minutes, planned or unplanned class, observed reason, evidence, recorder and review owner.
Can one stopped interval have more than one reason?
Yes, but overlapping reasons must not duplicate the same machine minutes. Keep supporting reasons on one event or split the interval using documented boundaries.
Does a missing machine signal mean downtime?
It means data is missing. Investigate connectivity, signal definitions and clock alignment before classifying the interval as a production stop.
Related Posts
Kanban System | Optiwise
Learn how a Kanban system works in manufacturing, where it helps, where it fails, and how Optiwise connects Kanban signals with inventory, purchase, and production planning.
12 Jun 2026Read more →Erp In Operations Management | Optiwise
Learn how ERP improves operations management by connecting planning, inventory, purchase, production, quality, dispatch, finance, and reporting.
12 Jun 2026Read more →ERP for FMCG Companies in India
A practical guide to ERP for FMCG companies in India, covering distributor orders, batch tracking, expiry, inventory, production, schemes, costing, and reporting.
11 Jun 2026Read more →
Optiwise, Odoo, Acumatica and Business Central for Manufacturing
Compare manufacturing workflows in Optiwise, Odoo, Acumatica and Dynamics 365 Business Central. See what your factory can run in Optiwise.
11 Jun 2026Read more →