Multi-Level BOM: Explosion Example and Revision Checklist
Multi-Level BOM. Use a worked manufacturing test, exception checks and direct Optiwise workflow evidence before rollout.
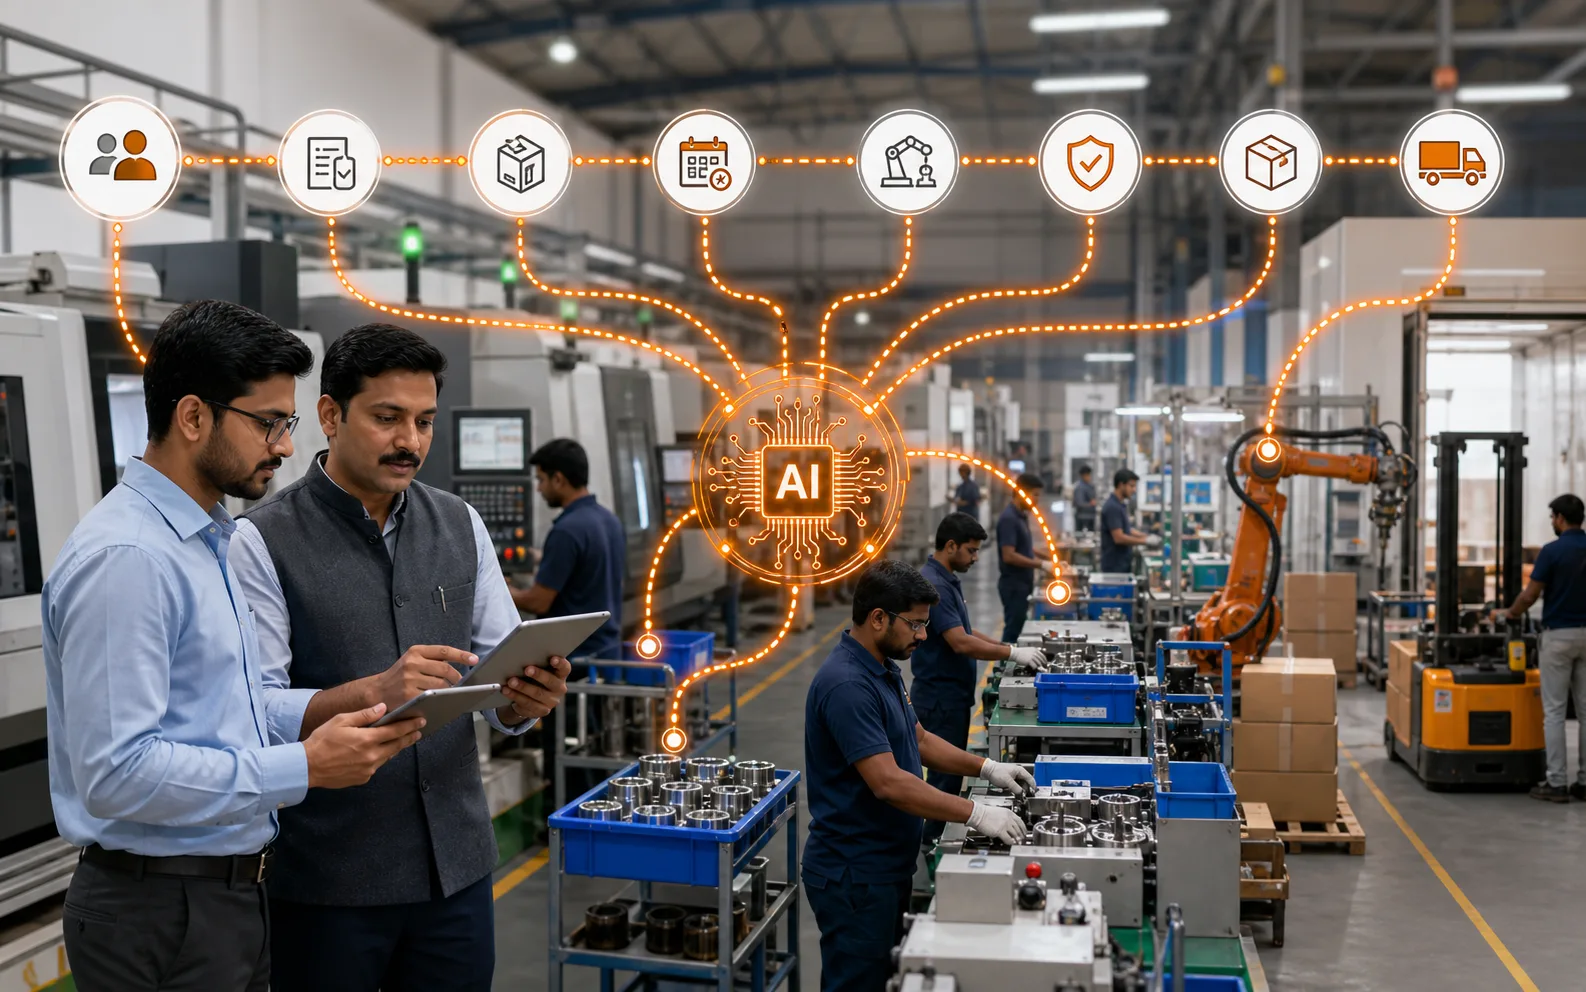
Multi-Level BOM: Explosion Example and Revision Checklist helps you plan subassemblies and components without losing revision control. Start with one order, one item and one exception. A screen tour cannot prove that records stay connected when the work changes.
Ten pumps need ten rotor assemblies. Each rotor needs one shaft and two bearings, so gross demand is ten shafts and twenty bearings before usable stock, open work and loss allowances are considered.
Start with the decision the system must support
Explode demand level by level, retain parent-child quantities and apply the approved revision to the correct orders.
Optiwise supports nested BOMs up to five levels, subassemblies, by-products, scrap, cost, separate routing and attachments, with Smart Suggest using BOM demand for action quantities.
Use ERPNext bill-of-materials documentation as an external reference for the relevant data or process model. It does not prove an Optiwise feature or a business result; the product statements above come from our current feature record.
| # | Input to prepare | Evidence to retain |
|---|---|---|
| 1 | Parent and subassembly codes | Owner and last update |
| 2 | Quantity per parent and UOM | Definition and source |
| 3 | Revision and effective order | Acceptance rule |
| 4 | Scrap, by-product and routing rules | Exception owner |
Run one controlled workflow before expanding scope
- 1. Parent and subassembly codes. Confirm who maintains it and which record is authoritative.
- 2. Quantity per parent and UOM. Use the current value in the chosen test order.
- 3. Revision and effective order. Record the pass condition before the demo begins.
- 4. Scrap, by-product and routing rules. Assign the person who resolves a mismatch.
Keep the first test small enough to reconcile by hand. When the system result differs from the source documents, stop and identify whether the problem is master data, timing, transaction ownership or configuration.
Test exceptions alongside the normal flow
- Subassembly has open stock
- Revision changes after release
- Alternate component needs approval
For each exception, record the expected status, permitted action, approver and audit trail. A useful manufacturing system should make the exception visible without allowing an unapproved shortcut to rewrite history.
Verify the connected Optiwise workflow
Review workflow details, product capability, supporting guide, implementation context, connected process, book a demo. In the demo, ask us to execute the scenario with your roles and sample records. Confirm the source transaction, resulting status, notification or action, correction method and report before accepting the workflow.
Questions to ask before rollout
What should we test first?
Choose one current order with a known complication. Prepare the four inputs above, run the transaction sequence and reconcile the result with the source documents.
What result should we accept?
Accept the workflow only when the normal path and named exceptions leave a complete, role-appropriate record. Keep feature validation separate from a promised business outcome.
A finished product often looks simple from the outside. Inside the factory, it may depend on dozens or hundreds of parts, subassemblies, bought-out items, consumables, and process steps. If this structure is not clearly defined, planning becomes guesswork.
A multilevel bill of material, or multilevel BOM, gives the business a structured map of the product. It shows not only the raw materials needed for the finished item, but also the subassemblies and child components required at each level.
For manufacturers, this matters because production, purchase, costing, inventory, and quality all depend on BOM accuracy. A system like AICAN Optiwise helps make BOMs usable in daily operations, not just technical documents stored somewhere.
What Is a Multilevel BOM?
A multilevel BOM represents a product in hierarchy. The finished product sits at the top. Below it are subassemblies, parts, raw materials, and sometimes further child levels. Each level contains item codes, quantities, units of measure, scrap allowance, alternatives if applicable, and sometimes operation linkage.
For example, a machine may include an electrical panel, frame assembly, motor assembly, fasteners, packaging, and documentation. The electrical panel itself may have its own BOM: enclosure, switches, wiring, connectors, labels, and bought-out components. A flat BOM would struggle to show this structure clearly. A multilevel BOM keeps the product logic intact.
Why Flat BOMs Create Problems
Many businesses start with flat BOMs in Excel. This works for simple products, but it becomes difficult as complexity grows. If a subassembly is used in multiple finished products, changes must be updated in many places. If one child part changes, teams may miss where it is used. Costing becomes inconsistent. MRP may calculate wrong requirements.
Flat BOMs also hide production reality. Subassemblies may be made in separate stages, stored as semi-finished goods, or outsourced. Treating everything as one raw material list makes planning weaker.
A multilevel BOM reflects how the factory actually builds the product.
How Multilevel BOM Supports Material Planning
MRP depends heavily on BOM structure. If the BOM is accurate, the system can calculate requirements across all levels. It can identify raw materials needed for subassemblies, semi-finished items needed before final assembly, and bought-out parts required at different stages.
This helps planners avoid missing lower-level requirements. In complex products, a small child component can delay the entire finished product. A multilevel BOM makes those dependencies visible early.
How It Improves Costing
Product costing becomes more reliable when the BOM structure is clear. Each level can carry material cost, process cost, subcontracting cost, scrap factor, and overhead assumptions. If a subassembly is common across multiple products, its cost can be maintained consistently.
This helps businesses quote more accurately, review margins, and understand cost impact when material prices change. Without BOM discipline, costing often depends on old spreadsheets and individual memory.
Engineering Changes and Version Control
Products change. A component is replaced. A supplier changes specification. A design team improves an assembly. A customer requires a variant. If BOM changes are not controlled, production may build from the wrong version.
A strong multilevel BOM process should include revision control, effective dates, approval workflows, and visibility into where-used relationships. This helps teams understand which finished products are affected when a component changes.
AICAN Optiwise can support structured manufacturing data so product definitions are connected with planning and production instead of being isolated in engineering files.
Supporting Subassemblies and Semi-Finished Goods
Many manufacturers build or procure subassemblies before final production. These subassemblies may have stock, quality checks, routing, and cost of their own. A multilevel BOM supports this by treating subassemblies as meaningful items, not just hidden lines.
This is especially important for machinery, electronics, automotive components, fabricated products, furniture, equipment, and any product with modular structure.
Common BOM Mistakes
The first mistake is not updating BOMs after production learns a better process. Engineering may define one structure, but the shop floor may use another. The system must reflect reality.
The second mistake is ignoring scrap or process loss. If actual consumption is higher than BOM quantity, material planning will always be short.
The third mistake is mixing substitute items without control. Alternatives are useful, but they should be defined properly.
The fourth mistake is allowing too many unofficial BOM versions. Teams must know which version is active.
Where Optiwise Helps
AICAN Optiwise helps manufacturers connect multilevel BOMs with material planning, production, inventory, costing, and purchase. This makes BOMs operationally useful. A planner can use them for MRP. Production can use them for work orders. Purchase can use them for material requirements. Management can use them for cost visibility.
A BOM should be the product truth. When it is accurate, every department works with better confidence.
Founder’s Note
At AICAN, we often see that product complexity is not the problem; invisible product complexity is the problem. Once the BOM is structured clearly, the factory can plan, cost, and produce with far less confusion. Optiwise is built to make that product structure visible and usable across the business.
FAQs
What is a multilevel bill of material?
A multilevel BOM shows a finished product as a hierarchy of subassemblies, components, and raw materials across multiple levels.
Why is multilevel BOM important?
It improves material planning, costing, production control, engineering change management, and visibility into product structure.
How is it different from a flat BOM?
A flat BOM lists all materials at one level. A multilevel BOM shows parent-child relationships and subassemblies.
Can multilevel BOM improve costing?
Yes. It helps calculate cost at subassembly and finished product levels more consistently.
Where can I learn more about AICAN?
Visit AICAN Optiwise and About AICAN.
Related Posts
Kanban System | Optiwise
Learn how a Kanban system works in manufacturing, where it helps, where it fails, and how Optiwise connects Kanban signals with inventory, purchase, and production planning.
12 Jun 2026Read more →Erp In Operations Management | Optiwise
Learn how ERP improves operations management by connecting planning, inventory, purchase, production, quality, dispatch, finance, and reporting.
12 Jun 2026Read more →ERP for FMCG Companies in India
A practical guide to ERP for FMCG companies in India, covering distributor orders, batch tracking, expiry, inventory, production, schemes, costing, and reporting.
11 Jun 2026Read more →
Optiwise, Odoo, Acumatica and Business Central for Manufacturing
Compare manufacturing workflows in Optiwise, Odoo, Acumatica and Dynamics 365 Business Central. See what your factory can run in Optiwise.
11 Jun 2026Read more →