Production Planning: Steps and a Worked Factory Example
Build a production plan from demand, BOMs, usable materials and available capacity. Follow a worked 120-unit job and a practical shift-plan checklist.
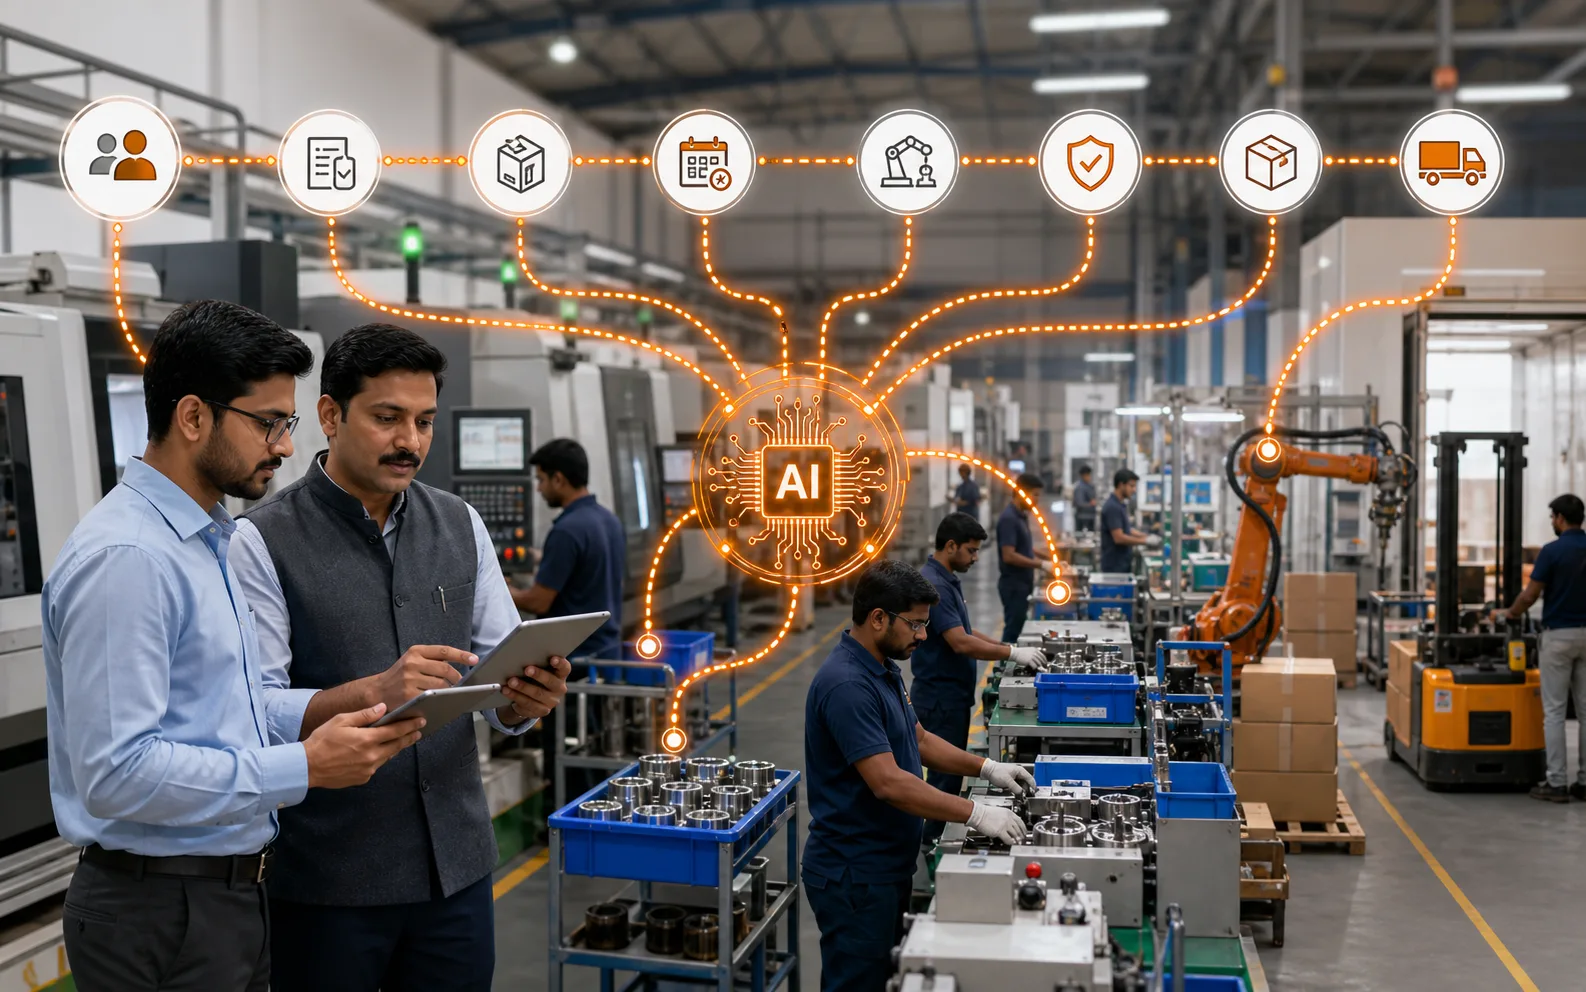
Production planning decides what to make, how much to make, when to make it and which materials, machines and people are required. A usable plan identifies the constraints before a job reaches the workstation.
Customer orders and forecasts describe demand. The planner turns that demand into proposed jobs, checks whether their materials and resources are available, and releases only the work that the factory can execute. The plan changes when a receipt is late, a machine stops or a customer revises a requirement.
Collect the inputs for one order
Start with an accepted quantity, drawing revision and required dispatch date. Use the approved bill of materials to identify components and the routing to identify operations. Record which materials are usable now, which are reserved for other jobs, and which are held for inspection.
For each operation, establish setup time, expected run time, the eligible machine, tooling and operator requirements. Separate processing time from waiting for an outside service, inspection or transport. An empty machine slot is unusable if the tool or trained operator is missing.
Work through material and capacity separately
Consider an illustrative order for 120 machined units. Each needs two minutes of machine time and the job needs one 30-minute setup. The machine has a 300-minute uncommitted window after breaks and existing work are accounted for.
| Input / result | Calculation |
|---|---|
| Run time | 120 units × 2 minutes = 240 minutes |
| Setup plus run time | 30 + 240 = 270 minutes |
| Uncommitted window | 300 minutes |
| Remaining time in that window | 300 − 270 = 30 minutes |
The job fits that machine window under these assumptions. The 30 minutes are a planning margin, not a promise of delivery. Inspection, handling, queueing and outside processes still need their own place in the schedule.
Now check material. If the job requires one blank per unit but only 100 usable, unreserved blanks are available, the shortage is 20. A purchase order due tomorrow does not make the full job ready today. The planner can wait, approve a technically valid partial batch, or evaluate another approved material source. Record the decision and its effect on the next operation.
Publish a plan people can act on
| Field | Example / acceptance check |
|---|---|
| Order, item and revision | 120 units; current drawing and BOM linked |
| Quantity released | Full 120 only after material check, or an explicitly approved partial quantity |
| Resource and window | Named machine, operator and 300-minute available window |
| Material exception | 20 blanks short; purchase owner and next confirmation time |
| Next operation | Inspection or outside process, with capacity and transfer time checked |
| Plan owner and version | Planner name, release time and superseded plan reference |
| Completion evidence | Good output, rejection, remaining quantity and actual finish |
Give stores, production and purchasing the same released version. A private spreadsheet updated after the work order has been printed can leave different teams following different plans. State where the approved plan lives and who communicates a change.
Replan when an assumption changes
If the receipt slips, check the jobs that depend on it and update their feasible start dates. If the machine loses 45 minutes before this job begins, its window falls to 255 minutes, below the 270 required. Review another machine, a revised quantity or a new completion commitment; do not keep the old finish time merely because it is already on the board.
Save the reason and the previous commitment. Track planned versus actual good output, late starts caused by material shortages, and jobs completed by the committed time. Compare like-for-like shifts and use consistent definitions for scheduled work and completed output.
ERPNext's production-plan documentation and work-order documentation provide examples of connected planning records. To assess Optiwise production planning, bring a job, its BOM and one actual constraint, then ask how the proposed configuration records the decision and communicates the revised plan.
Questions from manufacturing teams
What is the difference between production planning and scheduling?
Planning decides the quantities, resources and material needs. Scheduling assigns operations to specific resource windows. A feasible schedule must respect the constraints identified during planning.
Does enough machine time mean an order is ready?
No. Usable material, approved instructions, tooling, people and downstream operations must also be available. Check each constraint before releasing the job.
How often should a production plan change?
Review it at an agreed operating cadence and when a material, capacity or customer assumption changes. Publish a controlled revision instead of leaving conflicting versions in circulation.
Related Posts
A Manufacturing Alternative to SAP: Optiwise
Run your factory in Optiwise, a manufacturing alternative to SAP Business One with connected operations, AI agents and no-code workflows.
14 Jun 2026Read more →How Do I Know If My Manufacturing Business Really Needs an ERP?
A practical guide for manufacturers to identify when spreadsheets, manual follow-ups, and disconnected systems are no longer enough — and when ERP becomes an operational necessity.
14 Jun 2026Read more →Production Management System Optimized | Optiwise
Learn best practices for optimizing a production management system across planning, scheduling, material readiness, quality, and reporting.
12 Jun 2026Read more →
What Is the Best ERP for Pharmaceutical Manufacturing?
Learn how to choose the best ERP for pharmaceutical manufacturing, with guidance on batch control, quality workflows, traceability, inventory, documentation, and GMP discipline.
10 Jun 2026Read more →