
Capacity Utilization: Choose the Time You Are Measuring
Capacity utilization measures how much of a defined available capacity you used.

Capacity utilization measures how much of a defined available capacity you used. Use Optiwise machine calendars and recorded work to show the period, time basis and reason behind that percentage.
Name the denominator before comparing percentages
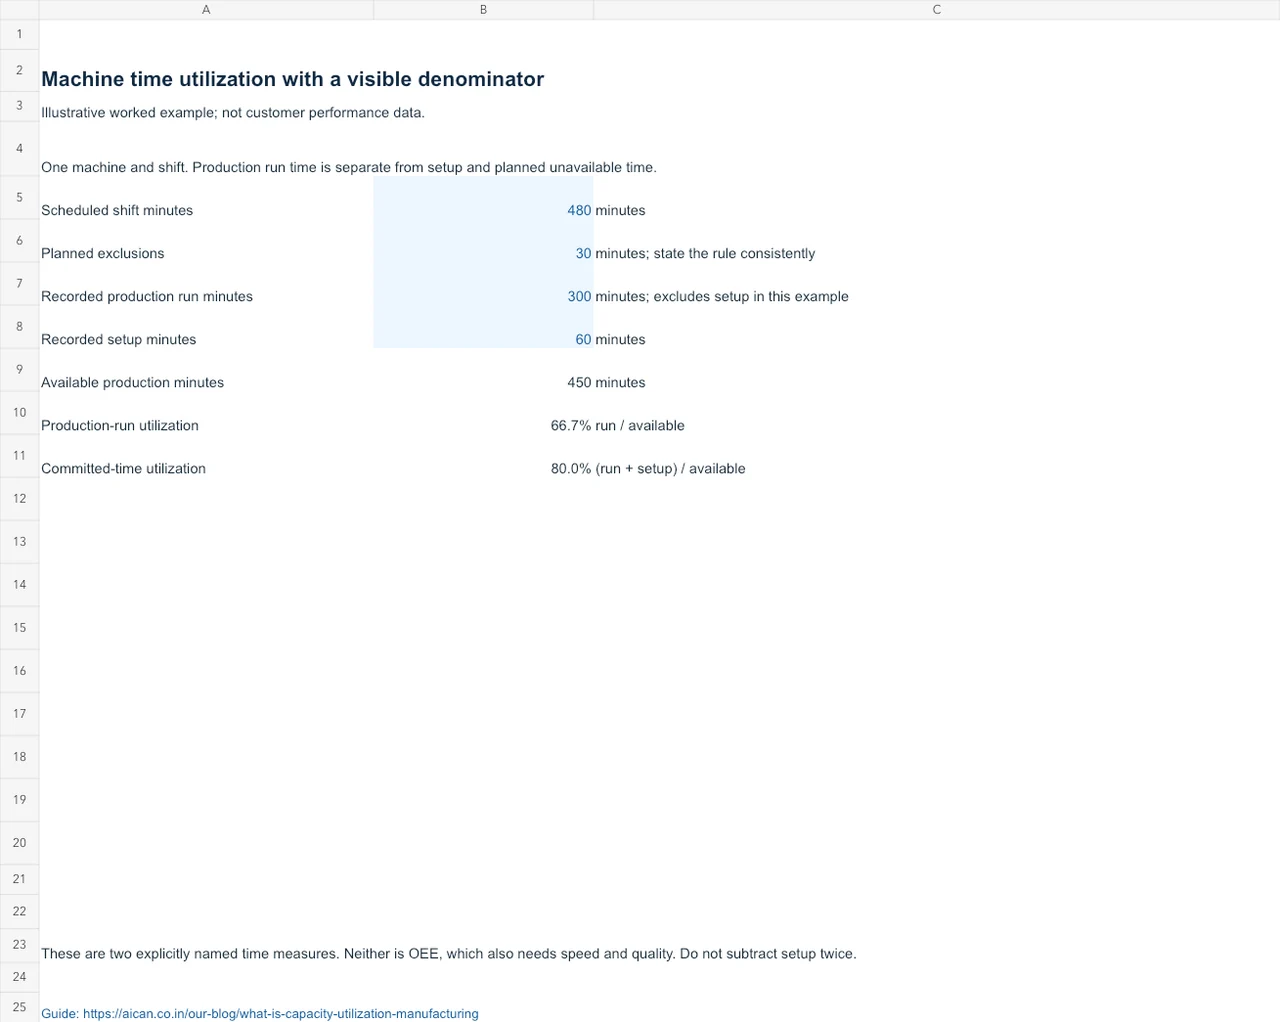
In this one-machine example, a shift has 480 scheduled minutes and 30 planned excluded minutes, leaving 450 available. Recorded production run time is 300 minutes, and setup is 60 minutes. Production-run utilization is 300 ÷ 450 = 66.67%.
If your decision is how much of the available shift was committed to setup plus production, the named measure is 360 ÷ 450 = 80%. Both are understandable when labelled. Calling both simply “utilization” hides the difference. Do not subtract setup from the denominator as well as including it in committed time.
Separate use, speed, quality and planned load
A running machine may be producing slowly or making rejected pieces. Overall equipment effectiveness, or OEE, combines availability, performance and quality; the OEE worksheet shows those inputs. The time ratios here do not calculate OEE.
Capacity requirements planning asks whether future load fits the calendar. It includes jobs already committed and the new operation’s setup and run time. A plan loaded above available hours is an overload; it does not prove that actual productive use exceeded physical time.
Follow the unused time to its cause
Our shop-floor records connect machine and worker assignments, time, quantities and operation outcomes. Connected IoT readings add machine information where the signal mapping exists; an operator may still need to explain a stop or setup. Check the latest reading before treating it as current production.
If usable material was missing, follow its receipt and quality status. If a fixture or skill was unavailable, revise that resource plan. If the machine had no work assigned, examine demand and scheduling. Keep the same period and time rule when comparing shifts or reviewing an investment; changing the denominator can create a better percentage without releasing any capacity.
Use the worked example with your own inputs
Download the editable Excel worksheet. It includes a worked example and a blank input sheet. Blue cells are inputs; formula cells calculate the result. The figures illustrate the method and are not customer results or an automatic Optiwise import.
Walk through the task in Optiwise
Bring one job or order and its difficult exception to a factory walkthrough. We will follow the inputs, action and resulting record together. Optiwise implementation costs ₹0. Subscription, optional add-ons and IoT hardware are separate.
Related reference: Odoo work-centre time and capacity configuration.

Related Posts

Kanban System | Optiwise
Learn how a Kanban system works in manufacturing, where it helps, where it fails, and how Optiwise connects Kanban signals with inventory, purchase, and production planning.
12 Jun 2026Read more →
ERP for Factory Operations: Follow Each Handoff
Follow a manufacturing order through material planning, buying, production, inspection and dispatch, with an owner for each delay or exception.
12 Jun 2026Read more →ERP for FMCG Companies in India
A practical guide to ERP for FMCG companies in India, covering distributor orders, batch tracking, expiry, inventory, production, schemes, costing, and reporting.
11 Jun 2026Read more →
Optiwise, Odoo, Acumatica and Business Central for Manufacturing
Compare manufacturing workflows in Optiwise, Odoo, Acumatica and Dynamics 365 Business Central. See what your factory can run in Optiwise.
11 Jun 2026Read more →