The Real Cost of Downtime in Manufacturing: A Checked Worksheet
Estimate downtime cost without double counting lost contribution, delayed recoverable output, overtime, scrap and fixed overhead.
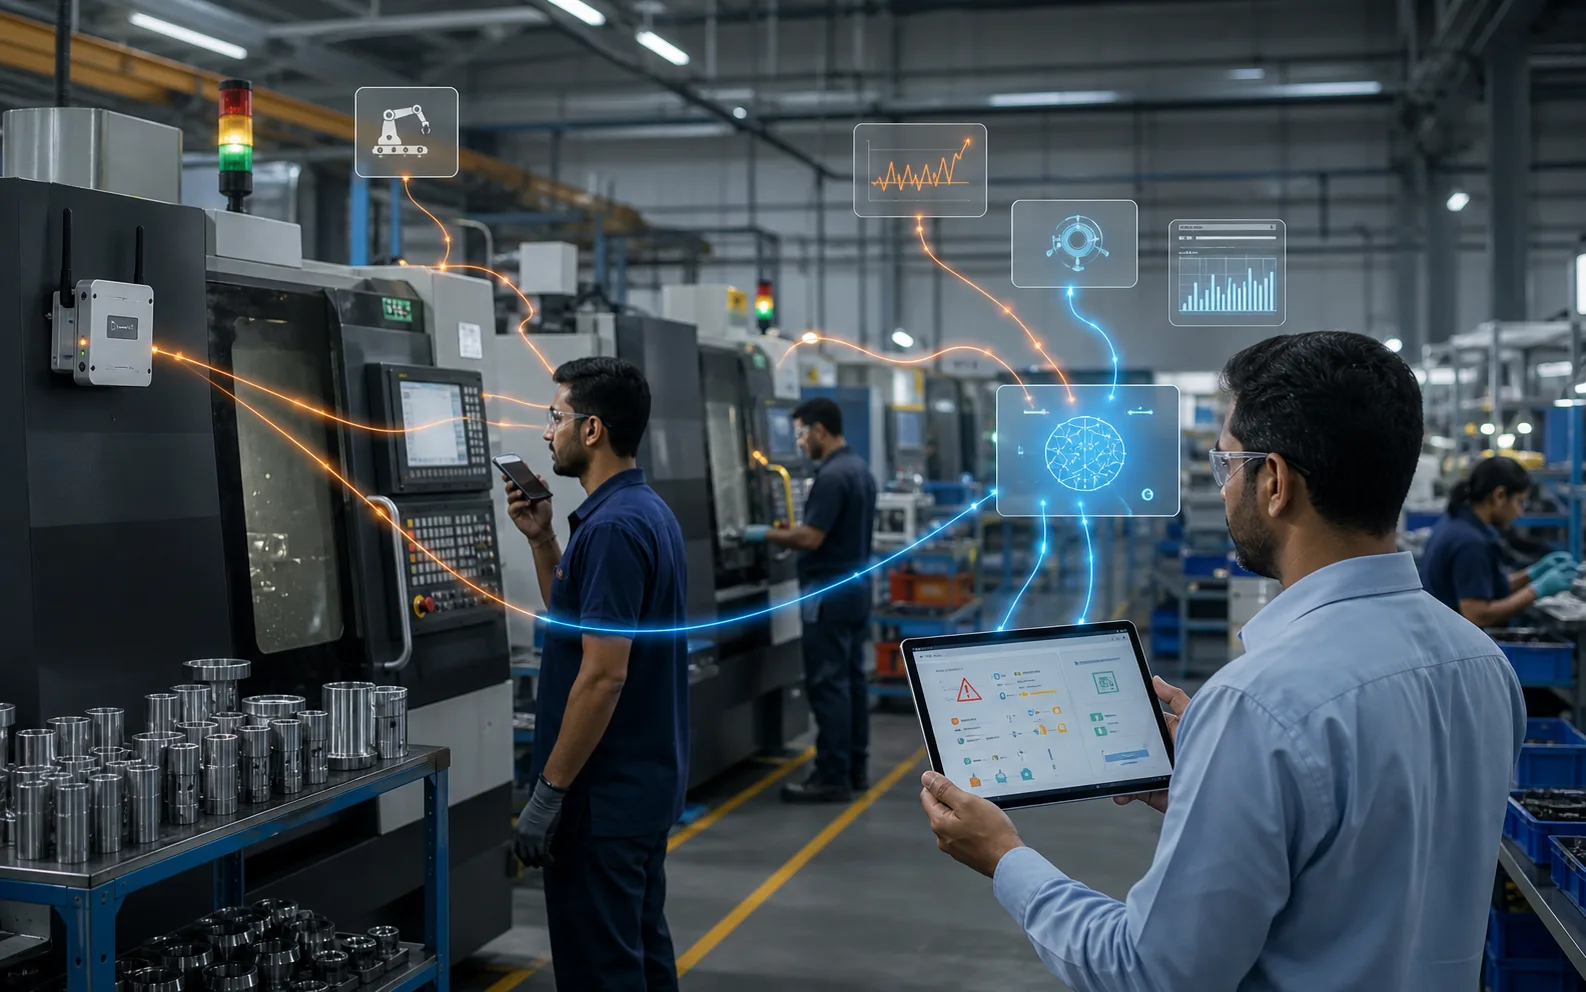
Downtime hurts factories in more than one way. The mistake is to multiply idle minutes by sales value and call that the loss. That number often double counts recoverable production and misses the real cost of overtime, scrap, missed dispatch and operator idle time.
Optiwise gives the production team the records needed to move from “machine stopped” to a checked cost view: planned time, running time, output, rejection, work order status and machine signal.
Direct answer
Downtime cost should separate lost contribution, delayed output, overtime, scrap, quality loss and overhead absorption so one stoppage is not counted twice.
Factory example
A bottleneck machine stops for 110 minutes during a priority batch. The team recovers half the output in overtime, so the worksheet records overtime cost for recovered output and lost contribution only for the unrecovered customer quantity. Restart scrap is recorded separately through quality disposition.
Implementation path in Optiwise
- Record planned time, actual stop time and reason.
- Separate recoverable delay from lost output.
- Attach overtime, scrap and quality loss only where the evidence exists.
Worksheet for your factory
Use this as the working checklist before you change software settings, write SOPs or ask the team to follow a new report.
| Record | What to capture | Why it matters |
|---|---|---|
| Lost contribution | Units that cannot be recovered multiplied by contribution margin | Use only for orders that are truly lost |
| Delayed output | Units recovered later | Record schedule impact, not lost revenue |
| Overtime or extra shift | Additional labour and utility cost | Count only if used to recover output |
| Scrap/rework | Material and process loss caused by restart or stoppage | Connect to quality disposition |
| Idle resources | Operators, tools or fixtures blocked by stoppage | Separate from machine hour cost |
| Fixed overhead absorption | Under-used planned capacity | Do not add if already included elsewhere |
How Optiwise supports this workflow
- Capture machine runtime, downtime and load using OptiEdge and related IoT records where the machine is connected.
- Compare planned output, actual output, rejection and rework in production dashboards.
- Connect stoppage reasons to work orders so supervisors can see which products, shifts and machines are affected.
- Use AI queries to ask which stoppage reasons are recurring and which orders were delayed because of them.
Explore the connected Optiwise workflows for production, inventory, purchasing, quality, IoT, and AI agents.
Checks before you use the number for decisions
- Confirm the owner of the record and the person who reviews exceptions.
- Write the unit of measure, time period and source system beside every number.
- Mark missing, stale or manually corrected data instead of hiding it inside the final score.
- Keep approval evidence for changes that affect stock, production, quality or customer commitments.
Reference source
For general manufacturing ERP and MRP context, compare this workflow with Deskera MRP resources, then adapt the records to your own factory process.
FAQs
What is the best first downtime cost metric?
Start with planned minutes lost by bottleneck machine, then attach contribution, overtime and scrap only where the evidence exists.
Should all downtime be converted into revenue loss?
No. Planned maintenance, recoverable delay and lost customer orders need separate treatment. The worksheet should show which cost line is proven and which one is only schedule impact.
Related Posts
Is AI Worth the Investment for My Factory?
Learn how to decide if AI is worth the investment for your factory by evaluating use cases, data readiness, costs, risks, ROI, and operational impact.
13 Jun 2026Read more →Manufacturing AI Mistakes to Avoid Before You Start
List manufacturing AI mistakes and controls for unclear use case, messy data, unsafe automation, no owner, weak security and unreviewed recommendations.
13 Jun 2026Read more →What's the Difference Between AI and Regular Automation?
Understand the difference between AI and regular automation in manufacturing, with practical examples for workflows, decisions, alerts, and predictive operations.
13 Jun 2026Read more →What Are the Risks of Using AI in Manufacturing?
Understand the risks of AI in manufacturing, including bad data, wrong recommendations, safety issues, security, job fear, over-automation, and implementation failure.
13 Jun 2026Read more →