Stock Availability: Calculate What You Can Promise
Separate on-hand stock, commitments, inspection holds and incoming supply. Use a worked manufacturing example before promising quantity and delivery.
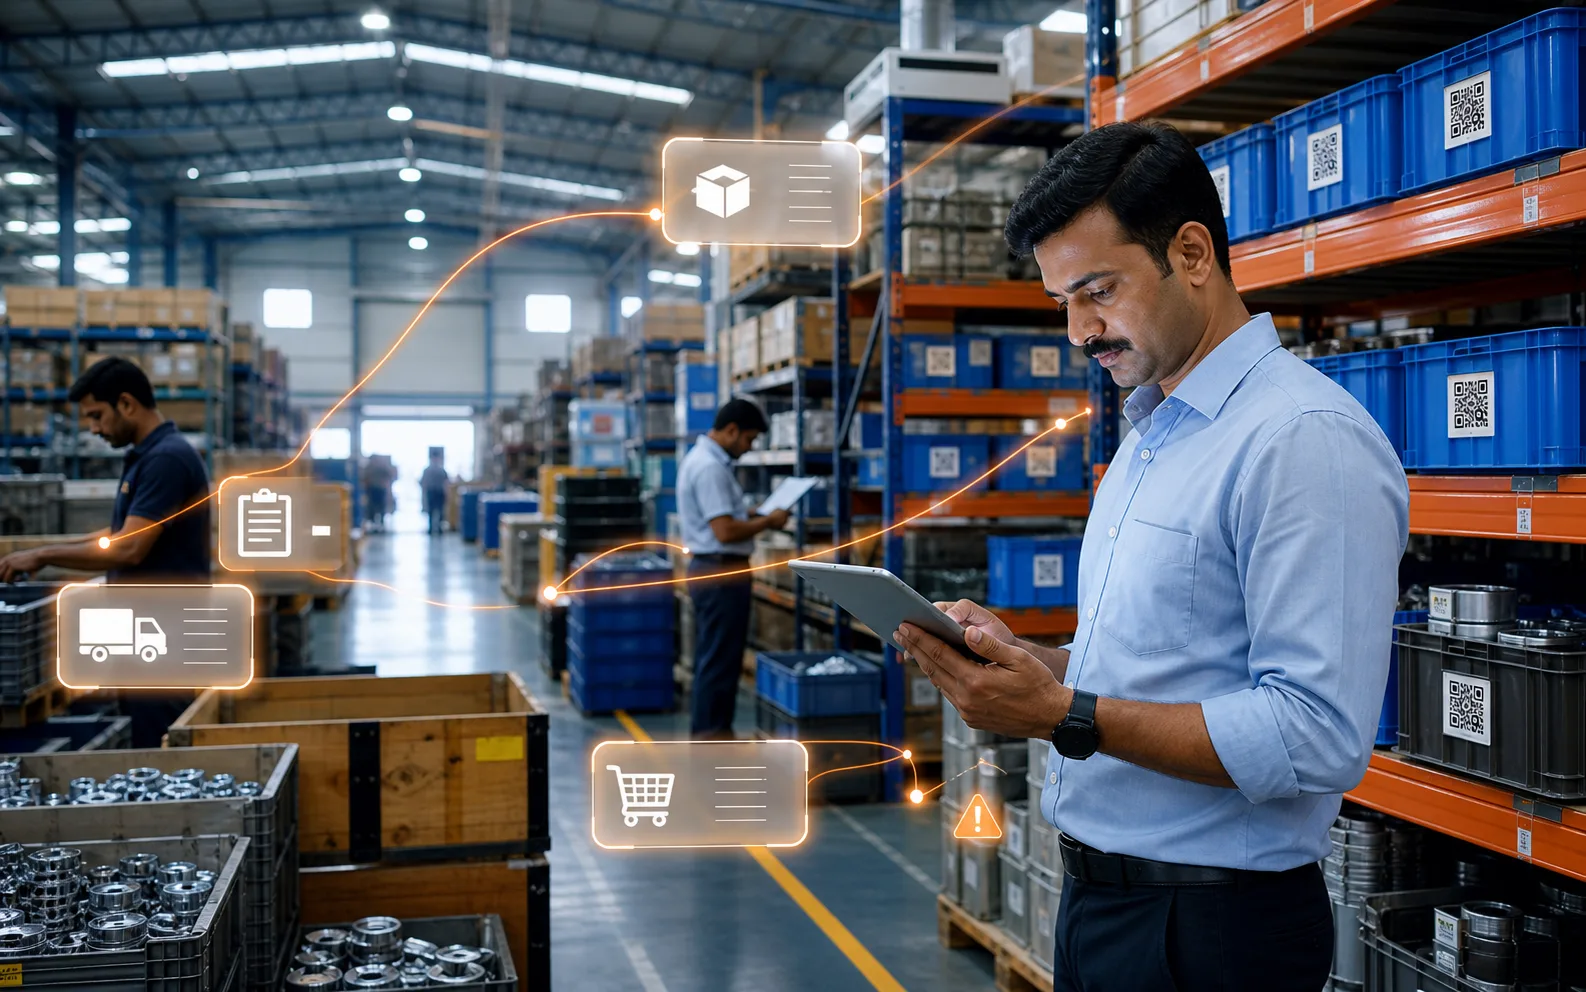
Stock availability is the usable quantity you can commit to a requirement at a stated location and time. Check existing commitments, quality restrictions and dated supply before treating an on-hand balance as available.
A customer asking for 500 pieces needs a quantity and a delivery date. “We have 650” is not enough if some pieces belong to another order or are waiting for inspection. Sales, stores and production need the same cut-off and status definitions when they make that decision.
Separate the stock you hold from the stock you can use
| Stock group | Pieces | Available for this new order? |
|---|---|---|
| Committed to an earlier order | 300 | No |
| Awaiting inspection | 100 | Not until accepted and released |
| Damaged and blocked | 50 | No |
| Uncommitted, accepted stock in the dispatch store | 200 | Yes |
| Total on hand | 650 | Only 200 available now |
The groups above are mutually exclusive. Available now = 650 − 300 − 100 − 50 = 200 pieces. A request for 500 therefore has a 300-piece gap. If a held batch is also reserved, assign it to a clear category or calculate the combined restriction once; subtracting the same pieces twice understates availability.
Put incoming supply on a date
Suppose a purchase order for another 400 pieces is due on Friday. It does not increase today's usable quantity. Record its expected arrival, receiving location, inspection requirement and other commitments. If the customer's dispatch is Thursday, that Friday receipt cannot support the promise.
For a later dispatch, check the supplier confirmation and the time needed for receipt and acceptance. An expected receipt is a planning input, not a completed receipt. The distinction between receipt and accepted or rejected quantities is also explicit in Frappe's purchase receipt documentation.
Use one availability record across the handoff
| Field | Decision it supports |
|---|---|
| Item, revision and unit | Are sales and stores discussing the same usable component? |
| Required quantity and date | What must be ready, and when? |
| Store and last update time | Is this balance current and at the right location? |
| Existing order commitments | Which quantities are already promised? |
| Inspection or damage status | Which pieces cannot yet be issued? |
| Incoming supply and readiness date | Can the gap be covered before dispatch? |
| Decision owner and next check | Who confirms the promise when an assumption changes? |
A transfer from another store needs its own movement and arrival time. WIP needs the remaining operations and inspection time. Substitute material needs an authorised technical decision. Keep each of those conditions attached to the proposed supply instead of folding everything into one optimistic number.
Connect availability to material action in Optiwise
Optiwise connects store movements, purchasing, production and quality records. Smart Suggest checks BOM demand against stock, open purchase orders and existing production, then gives the team action quantities for in-house work, buying or subcontracting. Purchase receipts follow the configured quality gates before accepted quantities become available.
Use that shared context alongside the confirmed customer requirement in sales/CRM. Review the material readiness checklist before releasing a job that depends on the shortage being filled.
Questions from manufacturing teams
Can pending inspection stock be promised as available now?
Keep it conditional until the authorised inspection and release are complete. If planning uses an expected release date, make that assumption explicit.
Should open purchase orders be added to on-hand stock?
No. Keep current stock and incoming supply separate, then assess whether the incoming quantity will be usable before the requirement date.
Why do two departments report different availability?
They may use different cut-off times, locations, units or commitment rules. Reconcile those fields before assuming that one report is wrong.
See the connected Optiwise workflow with an order, its stock position and the supply needed to cover the gap.
Related Posts
Is AI Worth the Investment for My Factory?
Learn how to decide if AI is worth the investment for your factory by evaluating use cases, data readiness, costs, risks, ROI, and operational impact.
13 Jun 2026Read more →Manufacturing AI Mistakes to Avoid Before You Start
List manufacturing AI mistakes and controls for unclear use case, messy data, unsafe automation, no owner, weak security and unreviewed recommendations.
13 Jun 2026Read more →What's the Difference Between AI and Regular Automation?
Understand the difference between AI and regular automation in manufacturing, with practical examples for workflows, decisions, alerts, and predictive operations.
13 Jun 2026Read more →What Are the Risks of Using AI in Manufacturing?
Understand the risks of AI in manufacturing, including bad data, wrong recommendations, safety issues, security, job fear, over-automation, and implementation failure.
13 Jun 2026Read more →