Takt Time Calculation: A Shift and Demand Worksheet
Calculate takt with matching shift and demand periods. Use a worked example to compare required pace, cycle time and changing product demand.
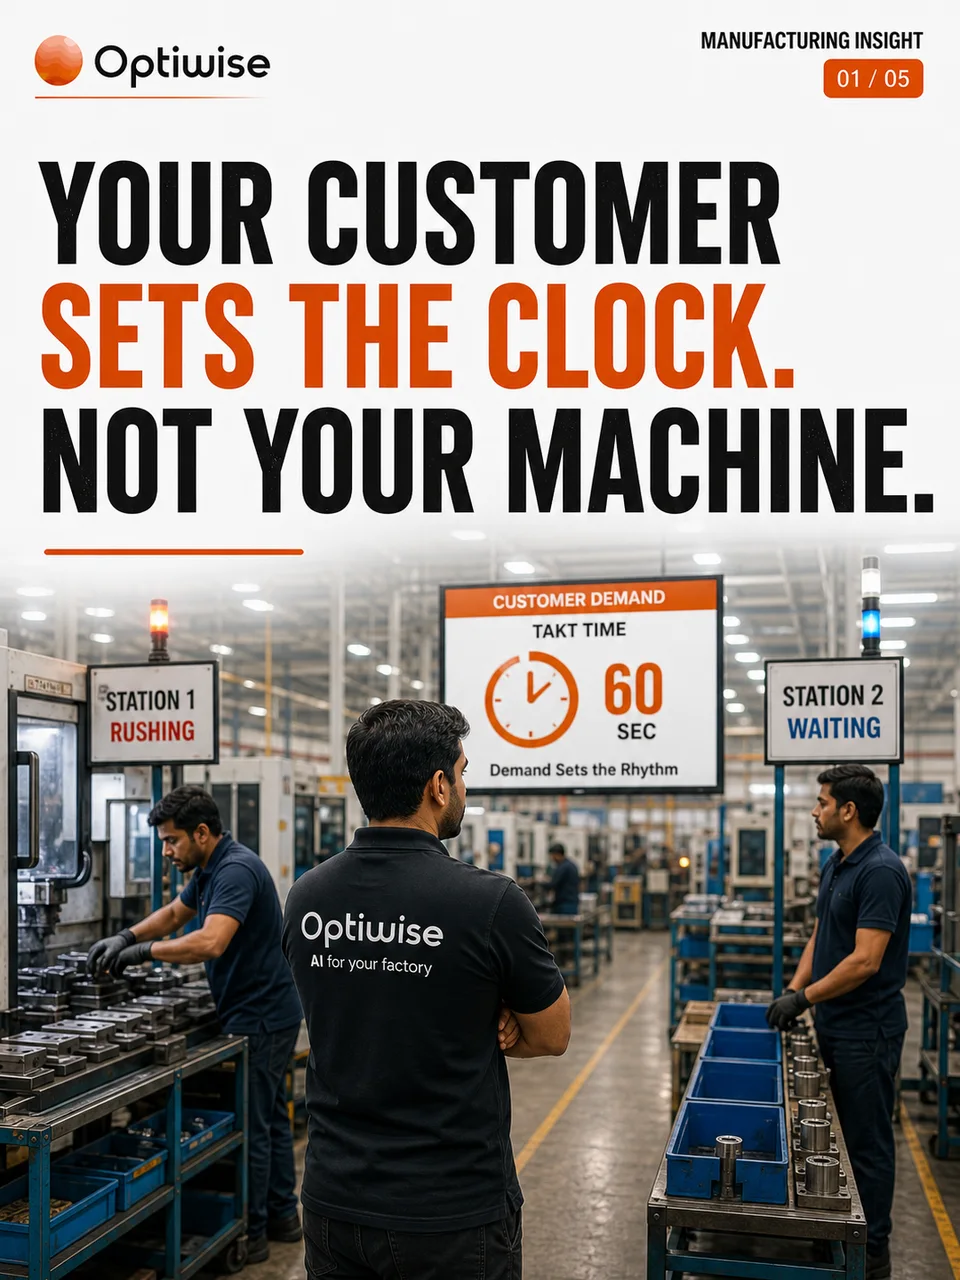
Takt time is the available production time for a defined period divided by customer demand for that same period. Use it to set the required output pace, then compare that pace with measured cycle times and the actual product mix before committing the schedule.
This worksheet is for the production planner and line supervisor when demand changes, an extra shift is proposed or a busy line keeps missing its dispatch quantity. Agree on the product family, demand window and time deductions before anyone calculates a target.
Lock the demand and time basis
Use an identified demand source, such as the approved daily requirement for one product family. Record its revision and the person who owns changes. Orders due this week cannot be divided by today's shift minutes unless the planner has explicitly allocated today's share.
The Lean Enterprise Institute defines takt as available production time divided by customer demand. The following numbers are an original illustrative scenario, not a measured factory result.
| Input | Value | Owner's check |
|---|---|---|
| Scheduled shift | 480 minutes | Supervisor confirms the calendar |
| Planned breaks | 40 minutes | Deduct once |
| Planned team meeting | 20 minutes | Confirm it is outside production time |
| Available production time | 420 minutes | 480 − 40 − 20 |
| Required good output | 350 units | Planner confirms this shift's demand |
| Takt | 72 seconds per unit | 420 × 60 ÷ 350 |
Write the formula with units. Dividing 420 minutes by 350 units gives 1.2 minutes per unit, which equals 72 seconds. A spreadsheet cell showing 1.2 without a unit is easy to misread as seconds.
Separate the required pace from the demonstrated pace
Suppose a station repeatedly takes 78 seconds per unit for this product under the measured conditions. Its theoretical output over 420 minutes is about 323 units before other losses: 25,200 ÷ 78 = 323.08. Demand requires 350. That comparison identifies a capacity question; it does not prove that asking the operator to work faster will close the gap.
Review the work content, material availability, tooling and upstream supply. If the measured cycle already includes a particular delay, do not subtract the same delay again from available time. Keep the observation method beside the result so the supervisor can reconstruct the comparison.
Use our line-balancing guide when deciding how tasks should be distributed. Takt establishes the demand pace; line balancing examines the work needed to meet it.
Check what changes when demand rises
If demand rises to 400 good units with the same 420 available minutes, takt becomes 63 seconds: 25,200 ÷ 400. The factory has not gained capacity because the target changed. The planner must show a feasible response, such as an approved change in work allocation, additional available time or a revised delivery commitment.
Do not multiply demand by a historical scrap percentage without stating whether the number represents expected input, attempted output or required good output. Keep the customer requirement and the internal allowance separate. Quality owns the validity of the allowance; the planner owns the commitment.
For a mixed-model line, a single average can hide a long-cycle variant. Keep a family-level takt only where it helps the flow decision, and also calculate workload from each variant's quantity and demonstrated time. A job shop may need an order-load schedule alongside any takt figure.
Use an exception log at the shift review
Record the required good output, actual good output, actual operating time and the reason for each material gap. Identify who can resolve each exception. A short shift, a machine loss and a demand change require different responses.
For the first week, accept the worksheet only if every shift uses matching time and demand periods, each deduction appears once, units are explicit and any station above the target interval has a named action. Recalculate when the approved demand or calendar changes. Retain the prior version so yesterday's plan does not appear to have used today's assumptions.
Connect demand, calendars and actuals in Optiwise
We connect production orders with machine calendars, shifts, worker availability and cycle-time planning in Optiwise. Manual worker or supervisor entries and industrial IoT capture supply execution data. You can retain this worksheet's assumptions in a configured form and compare the plan with the job's actual quantities and time.
Machine signals do not establish customer demand. Keep the commercial requirement linked to the plan and assign the planner to approve changes.
Questions about takt time
Is takt time the same as cycle time?
No. Takt is the pace required by demand. Cycle time measures how long the process takes under defined conditions. Compare them using consistent units and scope.
What if the demand is zero?
Do not divide by zero or assign an arbitrary takt. Record that no demand-based production pace is required for that period and review whether production should be released.
Bring one shift calendar and product-family demand plan to a demo, and we can connect the calculation to your production records.
Related Posts
Restart Dormant WIP: A Work-Order Release Checklist
Recheck held work before restarting: customer demand, quantity, identity, condition, revision and resources, with a worked WIP release example.
22 Sept 2026Read more →
Out-of-Tolerance Gauge: Trace and Contain Affected Product
Respond to a failed inspection gauge with an as-found record, affected-use timeline and separate quality decisions for stock and shipped goods.
22 Sept 2026Read more →
Material Substitution Approval: Request, Review and Release
Control proposed material substitutes with defined technical approval, quantity limits, issue records and treatment of unused alternative material.
22 Sept 2026Read more →Export Packing List: Reconcile Cartons Before Dispatch
Reconcile package contents, order quantities and weights before dispatch. Includes a mixed-carton example and controls for last-minute packing changes.
22 Sept 2026Read more →