Heijunka Planning: A Level-Loading Worksheet
Build a level-loading sequence from product mix, demand, setup time and due dates. Test an illustrative weekly plan against capacity and stock.
A heijunka schedule levels the volume and product mix released to production over a chosen period. Build it from demand, due dates, run times, changeovers and available capacity, then test whether the proposed sequence can meet each commitment.
This worksheet is for a planner managing a repeat product family that alternates between large queues and idle periods. Begin with one work centre and a short planning horizon. Keep unique engineered jobs and uncertain demand separate until their constraints are understood.
Choose the product family and planning window
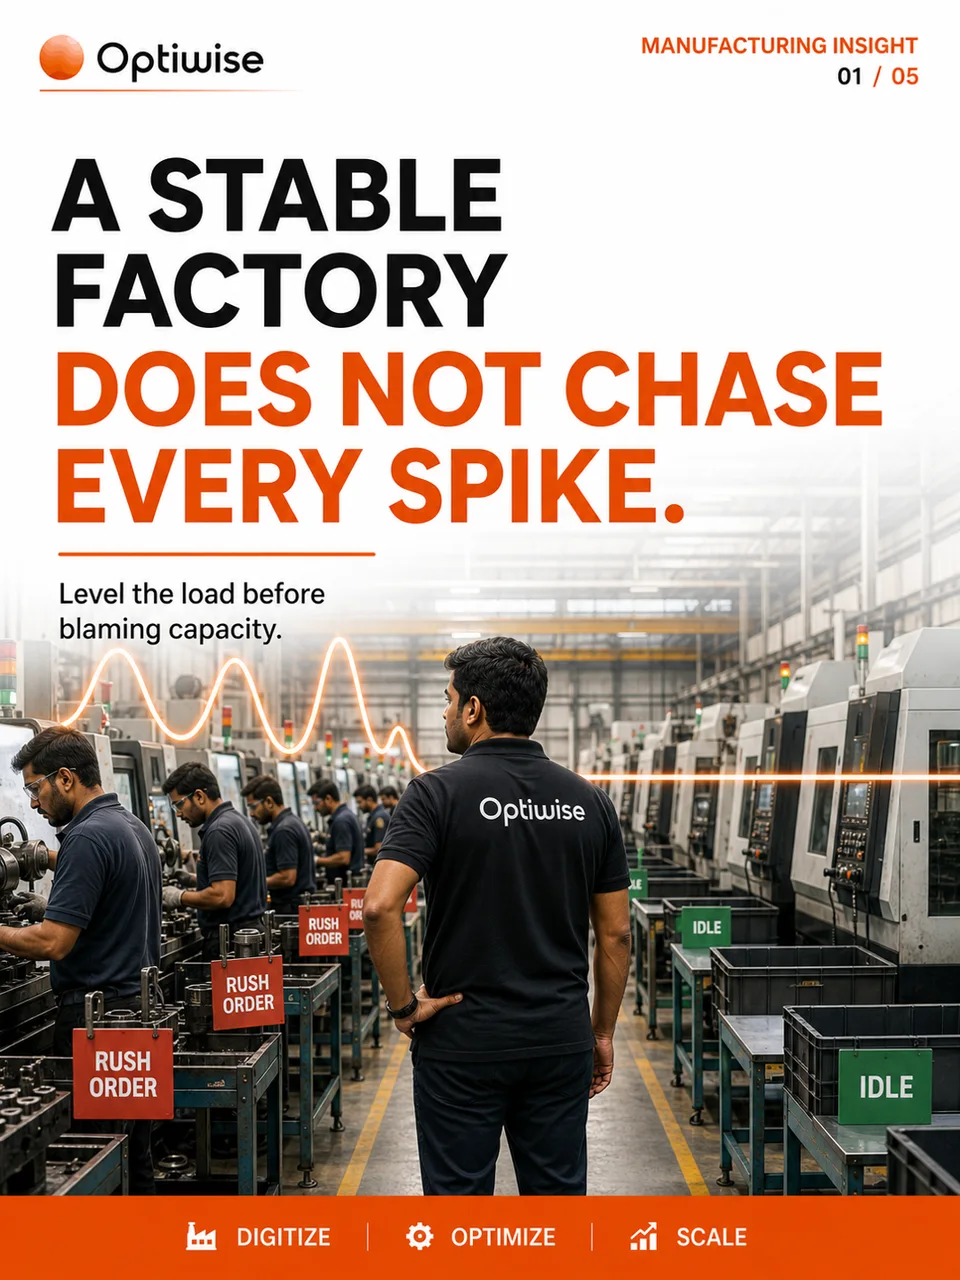
The Lean Enterprise Institute defines heijunka as levelling production type and quantity over a fixed period. Applying it requires checking both the repeated mix and the work needed to produce it. An equal unit count can still produce an uneven workload when products have different cycle times.
Collect accepted demand by item and due date, available finished stock, the intended inventory limit, net production minutes, actual run-time assumptions and the setup time for each transition. Check staffing, material and inspection capacity before reserving the sequence.
| Input | Product A | Product B |
|---|---|---|
| Weekly production requirement | 120 units | 80 units |
| Daily release over five days | 24 units | 16 units |
| Run time per unit | 3 minutes | 5 minutes |
| Daily run load | 24 × 3 = 72 minutes | 16 × 5 = 80 minutes |
Test the sequence against minutes and delivery dates
In this illustrative case, the daily sequence has 152 minutes of running. Assume the complete repeating sequence needs two transitions of 20 minutes each, including the return to the next day's starting setup. Total daily load is 152 + 40 = 192 minutes.
If the centre has 240 net available minutes after known exclusions, the schedule has 48 minutes unallocated. That margin is not additional promised output. The planner still needs to check normal variation, quality activities and any other shared constraints that were not included in the 192 minutes.
Now test a due-date exception. If a customer needs 40 units of B on Tuesday morning and there is no opening stock, Monday's 16 units are insufficient. A level daily average cannot satisfy that commitment. Review opening inventory, an earlier authorised release or an agreed delivery change before approving the plan.
Keep a cumulative line for each item: opening usable stock + completed accepted production − committed shipments. If it becomes negative at any dispatch boundary, revise the sequence. Also check that the projected stock never exceeds the approved holding limit.
Control changes to the released pattern
Define a frozen window for the pilot and name the person who can change it. When an urgent order enters, record what it displaces, the extra changeover load and which customer commitment needs review. Do not hide the disruption by leaving the original schedule unchanged.
If setup time makes the proposed pattern infeasible, test a longer repeating interval or work on setup preparation. Our SMED worksheet can help separate preparation from stopped-machine tasks. Do not remove necessary checks merely to fit more changes into the day.
Run the pilot with Optiwise planning records
We provide machine calendars, shift-based planning and production quantity entries in Optiwise production. Use those records to reserve the chosen sequence and compare actual completion with the released plan. The planner owns the levelling rule and its exceptions.
At each daily review, check due-date coverage, projected inventory, actual setup minutes and departures from the sequence. Accept the pilot only when each commitment is supported by the item-level balance and every sequence change has an owner. Compare several repeats before making a broader planning change.
Level-loading questions
Does heijunka mean making the same product every day?
No. The pattern depends on demand mix, setup constraints and the selected interval. Level both the required volume and the feasible product sequence.
Can a make-to-order factory use this worksheet?
Use it for repeat families where work content and demand are sufficiently understood. Check each order's due date and configuration; a stable average does not remove order-specific constraints.
Bring one week's accepted demand and setup records to an Optiwise planning demo to test a feasible release pattern.
Related Posts
Wet Bearing Packages: Receiving Hold and Release Checks
Record moisture-exposed bearing packages, hold affected stock and reconcile the authorised release or return without guessing product condition.
24 Sept 2026Read more →
Compressed-Air Leaks: A Repair and Verification Register
Turn a leak survey into prioritised repairs and verified closure. Includes a labelled energy-cost estimate and checks for measured savings.
24 Sept 2026Read more →
Machine Spare Transfers: Track Donor and Receiver Status
Approve both sides of a machine spare transfer, preserve component identity and assign donor restoration with a practical custody register.
24 Sept 2026Read more →
Temporary Approval Cover: Scope, Access and Handback
Set temporary approval boundaries, test access and reconcile the pending queue when cover ends. Use a worked handback balance and role checklist.
24 Sept 2026Read more →