Process Capability Study: Readiness Checks Before Cp and Cpk
Check stability, measurement, sampling and specification limits before calculating Cp and Cpk, with a worked example and review worksheet.
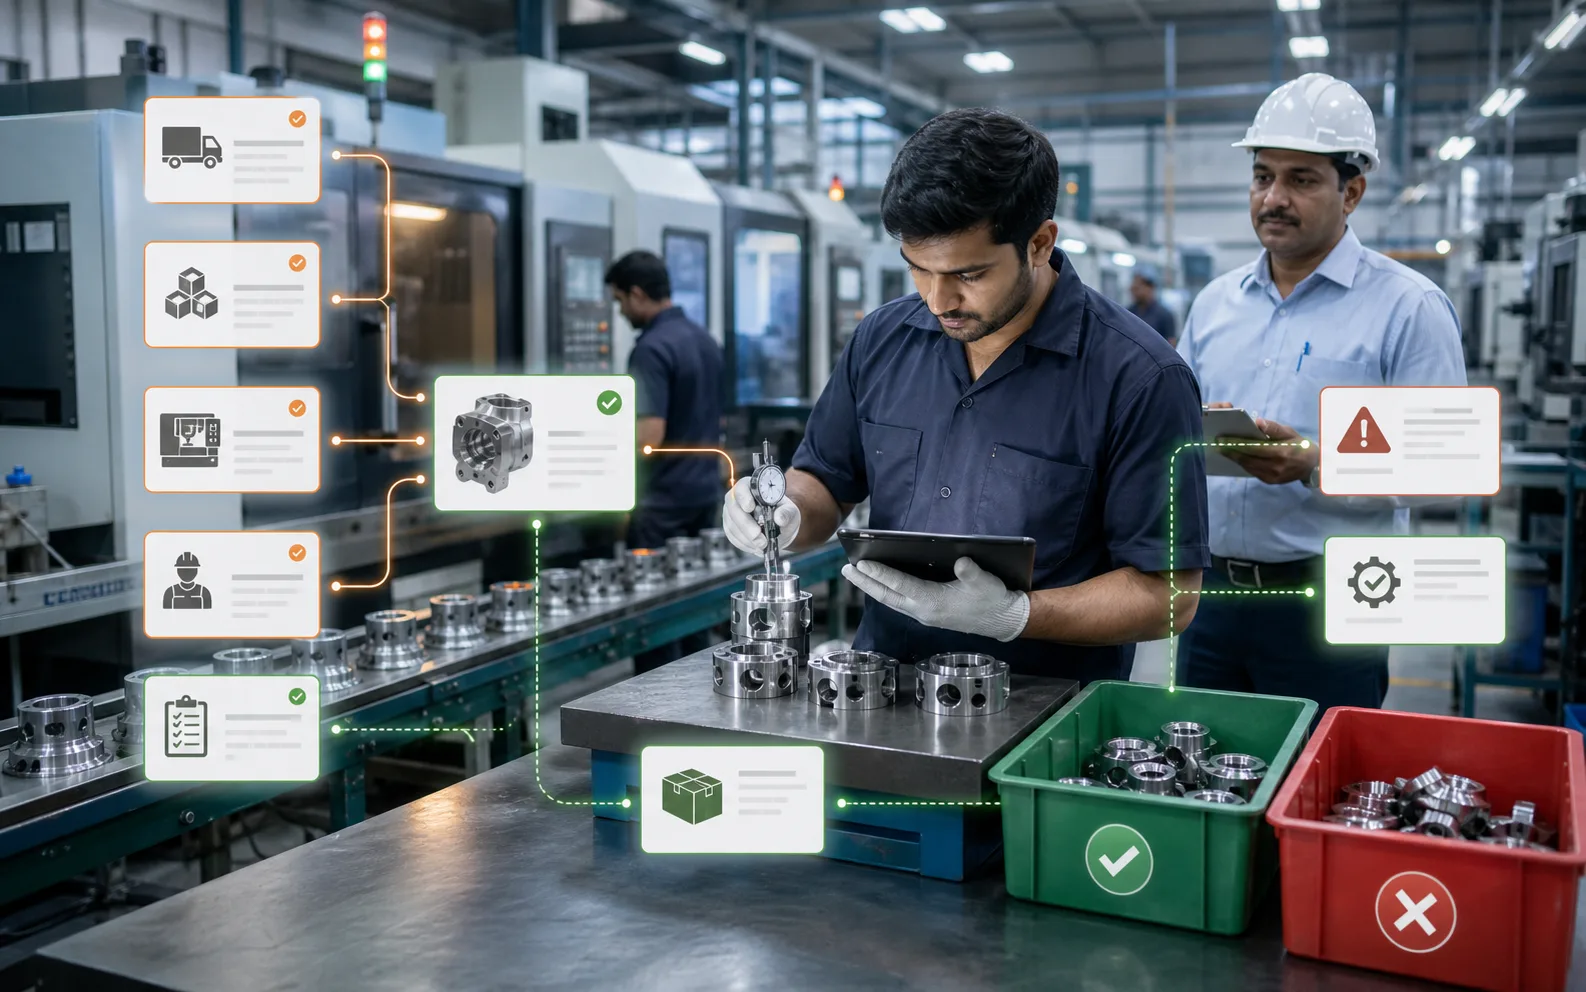
Calculate Cp and Cpk only after defining the characteristic and specification, checking the measurement method and establishing that the sampled process is stable. Keep the sampling conditions and variation estimate with the result so the number can be interpreted correctly.
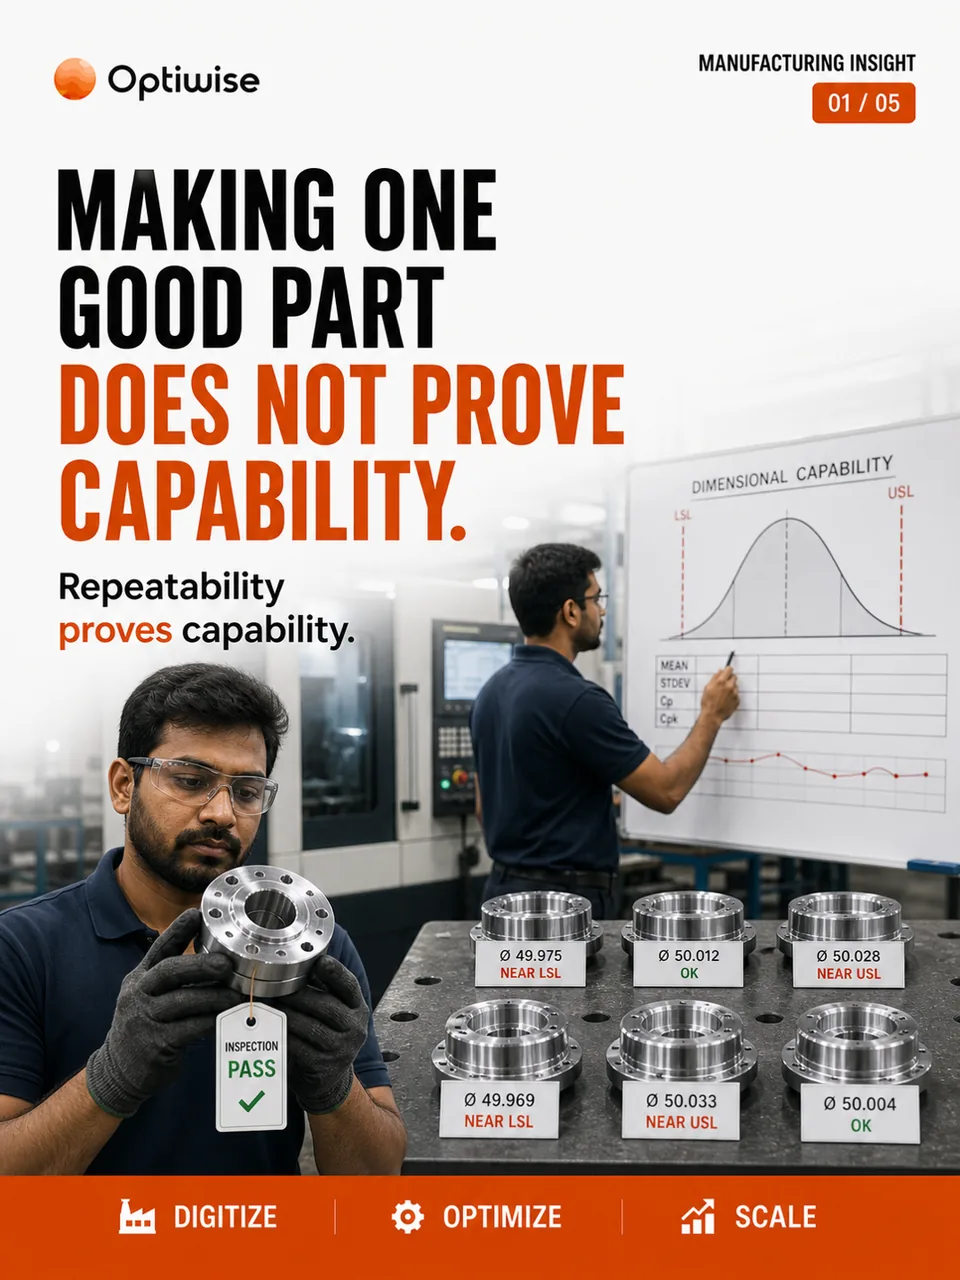
A customer asks for capability evidence on a bore diameter. The first inspected part is within tolerance, but that does not tell the quality engineer how the process behaves across time. A capability study needs a defined population of output, a defensible measurement method and a record of the conditions represented.
Write the study scope before collecting readings
Record the drawing revision, characteristic, units, upper and lower specification limits, machine, program, tooling, material and intended operating conditions. Name the quality engineer who owns the analysis and the process engineer who will investigate a signal. Keep acceptance criteria tied to the customer or internal requirement; do not choose a threshold after seeing the result.
| Gate | Evidence to retain | If missing |
|---|---|---|
| Specification | Approved limits, units and revision | Resolve the requirement before calculation |
| Measurement | Suitable instrument, method and measurement-system review | Review measurement error before attributing variation to production |
| Sampling | Time order, subgroup logic, quantity and operating coverage | Redesign the collection plan |
| Stability | Appropriate time plot/control-chart review | Investigate special causes; do not treat pooled data as a stable process |
| Model and estimate | Distribution assessment and stated variation estimator | Use an appropriate method with statistical support |
| Decision | Requirement, uncertainty and named reviewer | Keep the conclusion provisional |
NIST explains that process stability precedes capability analysis. Its capability guidance gives Cp and Cpk for a stable, normally distributed process and notes the importance of adequate independent data. A convenient handful of consecutive good parts is not a substitute for a planned study.
Work through the arithmetic, then inspect the assumptions
Illustrative calculation: a diameter has LSL = 19.90 mm and USL = 20.10 mm. Assume a justified study estimates mean = 20.04 mm and standard deviation = 0.02 mm, with stability and the model assumptions established. These invented values teach the calculation; they do not represent measured production.
Cp = (USL − LSL) / (6 × standard deviation) = 0.20 / 0.12 = 1.67. Cpk is the smaller of (USL − mean) / (3 × standard deviation) and (mean − LSL) / (3 × standard deviation). Here the two values are 0.06 / 0.06 = 1.00 and 0.14 / 0.06 = 2.33, so Cpk = 1.00.
The process spread fits more comfortably inside the specification width than its off-centre mean allows on the upper side. Reporting Cp alone would conceal that difference. Whether the study meets a requirement depends on the agreed criterion, uncertainty and validity of the study. Neither number authorises shipment of a nonconforming part.
Keep mixed conditions visible
A tool change, second cavity, different material lot or machine adjustment may change the process population. Record these events in time order. Decide with the quality engineer whether separate analyses are needed instead of pooling unlike conditions into one attractive average. Preserve excluded observations and the reason for exclusion.
For one-sided limits, non-normal data, autocorrelation or a changing process, the simple two-sided example may not apply. Use a suitable analysis rather than forcing the spreadsheet formula. Also state whether the reported variation is estimated within subgroups or across the overall study; otherwise two reports with the same label may describe different quantities.
Retain a reviewable study in Optiwise
Our configurable quality inspection forms collect the characteristic, result and supporting attachments. Custom process fields link study observations to production records. Retain the approved statistical analysis as an attachment; these data-capture capabilities do not imply that Optiwise calculates or certifies Cp and Cpk automatically.
Close the study only when another reviewer can reconstruct the limits, raw readings, sampling order, conditions, estimator and conclusion. Record any required centring or variation-reduction work separately, with a responsible engineer and a new verification plan.
Capability questions
Can first-piece approval replace a capability study?
No. First-piece approval records the checked setup and sample. Capability concerns the distribution of process output under defined conditions over the study.
Is 1.33 always the acceptance threshold?
No. Use the specified customer or internal requirement and the appropriate statistical interpretation. Do not insert a universal threshold into every study.
Show us your study record and inspection workflow in a demo.
Related Posts
Fabric Shade Groups: Allocate Rolls to a Cutting Lay
Allocate fabric rolls to cutting lays with shade-group approval, usable-length checks and remnant identity. Includes a two-group worked allocation example.
30 Sept 2026Read more →
Powder Coating Reclaim: Keep Each Blend Traceable
Build a powder-coating reclaim record with parent lots, approved blend rules, mass reconciliation and job links. Includes a clearly illustrative balance example.
30 Sept 2026Read more →
Torque Tool Job Changes: Record the Approved Setting
Use a torque-tool job-change record to connect joint revision, units, tool identity, setup verification and the first affected assembly without inventing settings.
30 Sept 2026Read more →
Opened Adhesive Containers: Record Dates Before Reissue
Track partially used adhesive containers with opening dates, supplier limits, storage exceptions and an issue-return worksheet. Avoid invented expiry extensions.
30 Sept 2026Read more →