SPC Reaction Plan: Respond to a Control Chart Signal
Build an SPC reaction plan with signal evidence, affected-output boundaries and release checks. Includes an illustrative control-limit example.
An SPC reaction plan specifies what to do when a control chart signals a process change: preserve the measurements, check the signal and measurement system, identify affected output, investigate the cause and record the authorised response. Control limits and product tolerances serve different purposes.
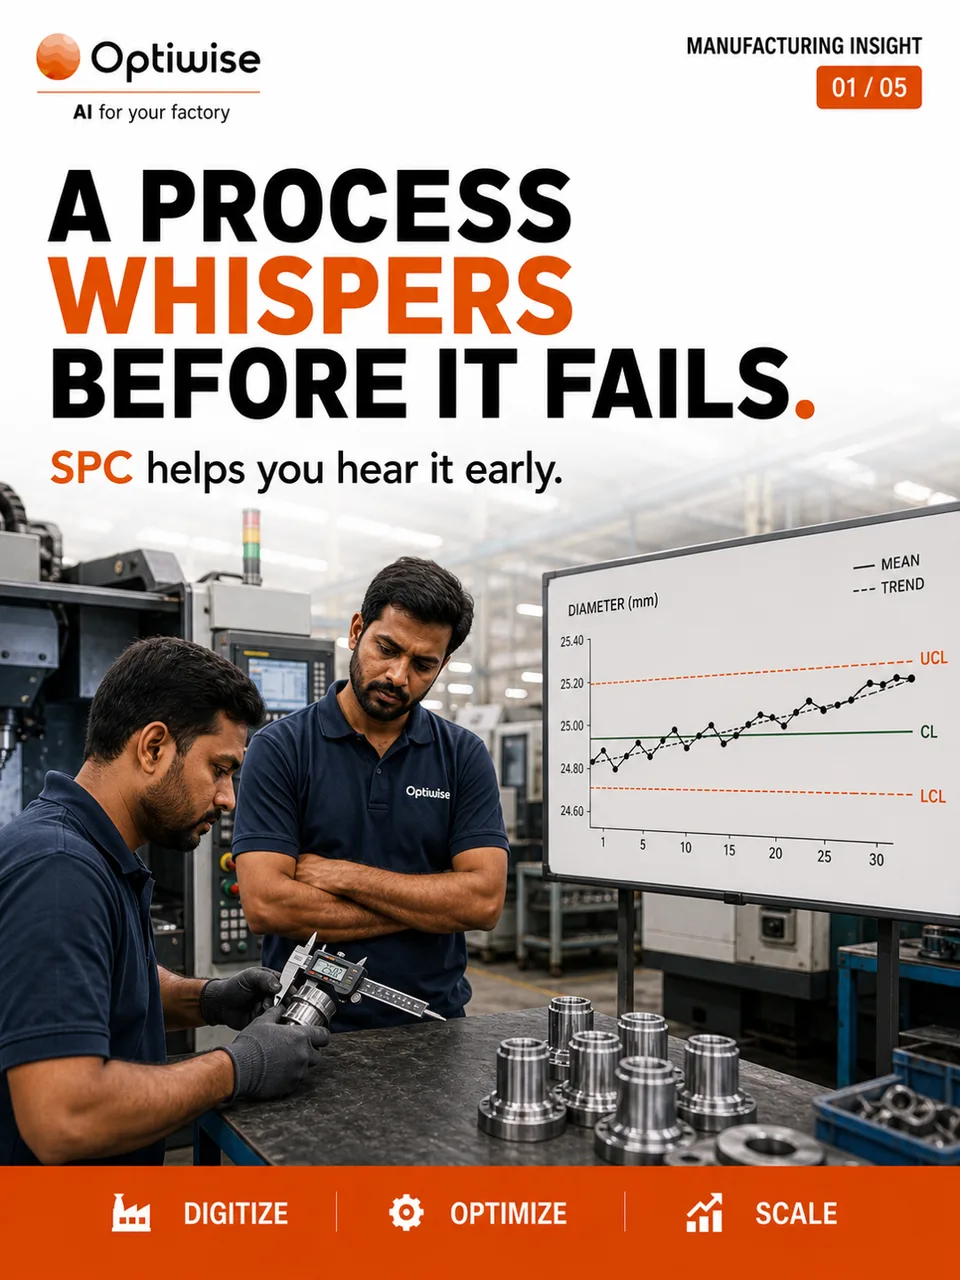
The chart has a point beyond its upper control limit, but the measured dimension is still inside the drawing tolerance. The operator needs a defined response. Adjusting the machine by habit can erase the conditions the quality engineer needs to investigate.
Separate the process signal from product acceptance
NIST’s control-chart guidance describes monitoring process behavior over time against a center line and control limits. A signal calls for investigation. Product specification limits come from the applicable requirement; they are not substitutes for control limits calculated for the chosen chart.
Illustrative scenario: an approved individuals chart has a center line of 20.00 mm and control limits of 19.97 and 20.03 mm. The product tolerance is 19.90–20.10 mm. A reading of 20.04 mm is inside the product tolerance and beyond the chart’s upper control limit. It does not prove that the part is defective, and it does not justify ignoring the process signal.
The numbers are assumed for explanation. They are not limits to copy into a live process. Your quality engineer selects the chart, baseline, subgroup method, sampling interval and signal rules for the actual data. Use our process-capability readiness guide when the next question is whether a stable process can meet tolerance.
Write the response before the next signal
| Stage | Required record | Owner and decision |
|---|---|---|
| Detect | Characteristic, chart version, timestamp and rule triggered | Operator preserves the original reading |
| Check | Instrument ID, method, transcription and sample identity | Quality checks whether the signal is valid |
| Bound output | Last supported stable point, intervening output and locations | Quality defines containment and review scope |
| Investigate | Changes in tool, material, setup, method and environment | Process owner records evidence and cause hypothesis |
| Respond | Approved correction, verification data and unresolved risks | Authorised reviewer records continue, hold or restart |
| Close | Release reference, affected-output disposition and follow-up | Quality confirms all open branches have an owner |
A production supervisor should know the stop or hold rule in advance. Some processes require immediate interruption; others permit a defined investigation while product remains controlled. The plan must name the decision authority and the production restrictions. An unanswered call does not grant permission to continue.
Preserve evidence before changing the process
Keep the original point, its time and the underlying sample readings. A repeat measurement may help investigate the gauge or method, but it must not silently replace an inconvenient result. Record who repeated it, how and why. If a decimal or unit was entered incorrectly, retain the correction trail.
Identify the parts made between the last supported process condition and the response. Use the work order, tool or cavity, material lot and output locations to define that boundary. A sample that passes tolerance does not by itself release every part in the interval. Quality chooses the appropriate product review and records the disposition.
Check recent changes in the order they occurred. For example, a tool replacement followed by a fixture adjustment and a material-lot change creates three separate investigation leads. Avoid rewriting the control limits to absorb the new point. A revised baseline needs a justified process change and qualified review.
Accept the response through evidence
The event can close when the signal is explained or has a documented investigation outcome, affected output is accounted for, the approved response is recorded and the required verification readings are available. Keep the restart authority separate from the person who performed the adjustment where your control plan requires it.
Set a follow-up review for the next comparable run. Check whether the same signal or cause recurs and whether operators followed the response. A chart with fewer recorded signals is not an improvement if measurements were skipped.
Capture the reaction record in Optiwise
We support parameterized quality inspection, configurable QC forms, conditional fields and role-based form access. You can configure the signal record, required attachments and response owner alongside production process entries. The chart method and statistical interpretation remain part of your approved quality procedure.
SPC response questions
Does an out-of-control point mean the product is out of specification?
No. The chart evaluates process behavior, while specifications define product acceptance. Investigate the signal and assess affected output under the quality plan.
Should we recalculate limits after every signal?
No. Preserve the approved limits while investigating. A new baseline requires a justified review of process conditions and suitable data.
Bring a control plan and one signal record to an Optiwise demo to map the inspection and response workflow.
Related Posts
Fabric Shade Groups: Allocate Rolls to a Cutting Lay
Allocate fabric rolls to cutting lays with shade-group approval, usable-length checks and remnant identity. Includes a two-group worked allocation example.
30 Sept 2026Read more →
Powder Coating Reclaim: Keep Each Blend Traceable
Build a powder-coating reclaim record with parent lots, approved blend rules, mass reconciliation and job links. Includes a clearly illustrative balance example.
30 Sept 2026Read more →
Torque Tool Job Changes: Record the Approved Setting
Use a torque-tool job-change record to connect joint revision, units, tool identity, setup verification and the first affected assembly without inventing settings.
30 Sept 2026Read more →Opened Adhesive Containers: Record Dates Before Reissue
Track partially used adhesive containers with opening dates, supplier limits, storage exceptions and an issue-return worksheet. Avoid invented expiry extensions.
30 Sept 2026Read more →