Release Corrugated Cartons Against the Right Test Results
Connect corrugated-carton lots to the right quality tests. See why matching GSM cannot replace missing board or box results before release in Optiwise.
Release a corrugated-carton lot against the test results required by the customer’s specification. In Optiwise, we connect the job, material lots and quality record so a matching paper weight does not stand in for missing board or finished-box evidence.
GSM means grams per square metre: the mass of a stated paper or board area. A supplier’s paper GSM, the basis weight of the combined corrugated board and the performance of the finished carton describe different things. Start by identifying which material or product the requirement refers to.
Match the test to the question you need to answer
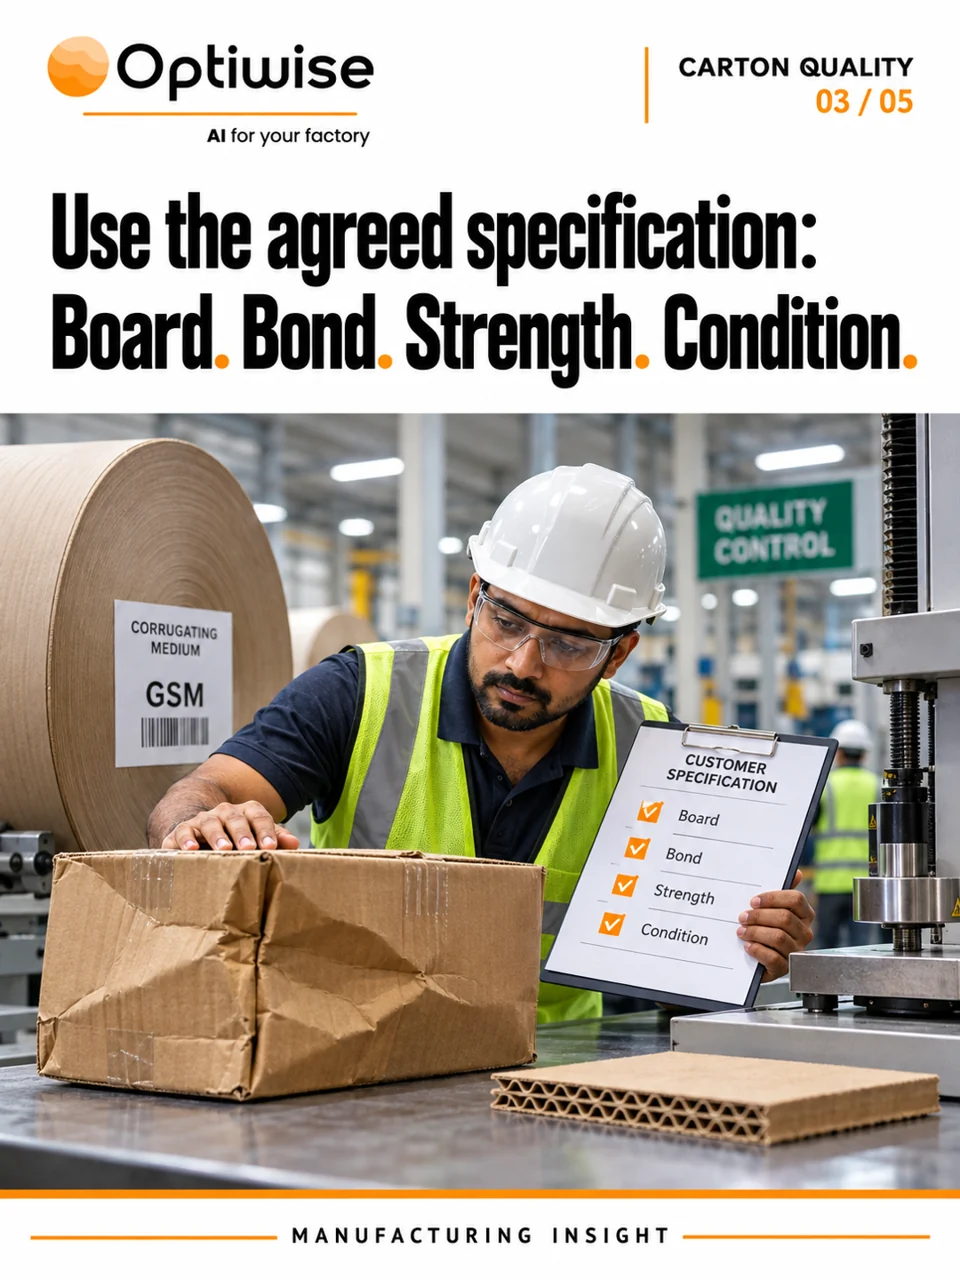
FEFCO’s testing-method list separates basis weight, edgewise crush resistance, glue-bond tests and packaging compression resistance. These are different measurements. A satisfactory weight result cannot supply a missing strength or bonding result.
| Record | What it addresses |
|---|---|
| Component-paper basis weight | Mass per area of the specified paper |
| Board edge-crush result | Resistance of the tested board edge under the stated method |
| Glue-bond result | The specified bond property under its test method |
| Finished-box compression result | Compression performance of the tested packaging under stated conditions |
Your customer’s agreed specification determines the applicable tests, sample preparation, conditioning, units and acceptance limits. Select the tests required by the agreed specification. Keep the sample and test conditions with the result, particularly when the carton’s use includes stacking, moisture exposure or a specific packed load.
SATRA’s carton-assessment guidance also treats weight, edge crush and box compression as separate properties and discusses how the packaging and its contents affect stacking assessment. Use the method and conditions appropriate to the product you are supplying rather than calculating a universal stacking limit from GSM.
Put the required evidence on the production job
In Optiwise, keep the customer’s product and specification reference with the job and its material and process instructions. Record the paper or board items and lots issued to that work. If an artwork, board construction or required test changes, identify which revision the released job is following before another team uses an old instruction.
Configure the inspection form and quality process for that customer requirement. A useful result record identifies the job and production lot, specification revision, sample reference, test method, result and unit, test date, responsible person and supporting report. Include the conditioning or sample details required by the agreed method.
The laboratory or authorised tester performs the test. Your quality user enters the result and attaches the report in the configured form, then records the outcome through the quality workflow. Keep the instrument and sample references required by your test procedure with that evidence.
Keep a missing result separate from an accepted lot
Consider an illustrative order with two lots of the same carton design. Lot C-61 contains 600 cartons and Lot C-62 contains 400. Their paper specification carries the same GSM. The agreed release requirements include a specified edge-crush result and a finished-box compression result.
C-61 has its paper-weight and edge-crush records, but the required finished-box result is missing. C-62 has the required results, and the authorised quality user has accepted that lot under the customer’s rules. There are 1,000 cartons physically present, 400 accepted for this decision and 600 awaiting the missing evidence. The matching GSM does not transfer C-62’s acceptance to C-61.
Record C-61’s outstanding test, the person responsible and the next action. Keep the lot distinguishable while the evidence is obtained. Production and dispatch should use the accepted quantity when reviewing the delivery commitment, rather than treating “manufacturing complete” as “released”. A release may also depend on other agreed checks, such as artwork or dimensions.
Resolve a failed test against the affected lot
If C-61 later fails the required test, retain the actual result and its conditions. Quality decides the disposition under the customer’s specification and the factory’s approved process. Record the affected quantity and whether further assessment, rework or rejection is authorised. Do not change the requirement or attach C-62’s report to make the pending line disappear.
When additional samples or retesting are permitted, retain their relation to the original lot, result and authorised decision. A test on a new sample does not by itself erase the first failure or prove every carton is acceptable. The responsible quality team determines what the evidence allows.
Our production records retain the material issues, process quantities and job context behind that investigation. The inventory movement history connects the physical lot with its receipt, issue or transfer. We configure the required fields and inspection steps around your product and customer requirements, keeping the next decision connected to the same work.
Questions about GSM and carton release
Does matching GSM prove a corrugated carton is strong enough?
No. GSM describes mass per area of the stated paper or board. Use the customer-required board and finished-box tests to assess the relevant performance, with the specified sample conditions and limits.
Can we use another lot’s report if the paper specification is the same?
Only where the agreed specification and sampling rules allow that evidence to represent the lot. Do not assume that matching GSM or design makes two production lots interchangeable for release.
Bring one carton specification, two production lots and a missing-test exception to an Optiwise walkthrough. We will connect the job, material record, inspection evidence and dispatch decision.
Related Posts
Find the Bad Mould Cavity Hidden in Your Reject Total
Compare injection-moulding rejects by cavity within the same run. Use a worked sample, clear denominators and linked quality records in Optiwise.
1 Nov 2026Read more →How Sensors Help With Quality Control in Manufacturing
Explain quality-control sensors through measured property, tolerance, calibration evidence, sampling, false alerts and human disposition.
11 Jun 2026Read more →
Track Quality Issues in ERP: Inspection to Disposition
Follow an inspection issue through stock hold, approved rework or scrap, quantity reconciliation and corrective-action checks, with a 50-part example.
28 May 2026Read more →
Use IoT readings alongside quality and job records
Connect machine signals with job and inspection context in Optiwise. See how to investigate a changed reading without treating it as proof of a defect.
13 May 2026Read more →